CategoriesERP (Enterprise Resource Planning) ERP Solutions

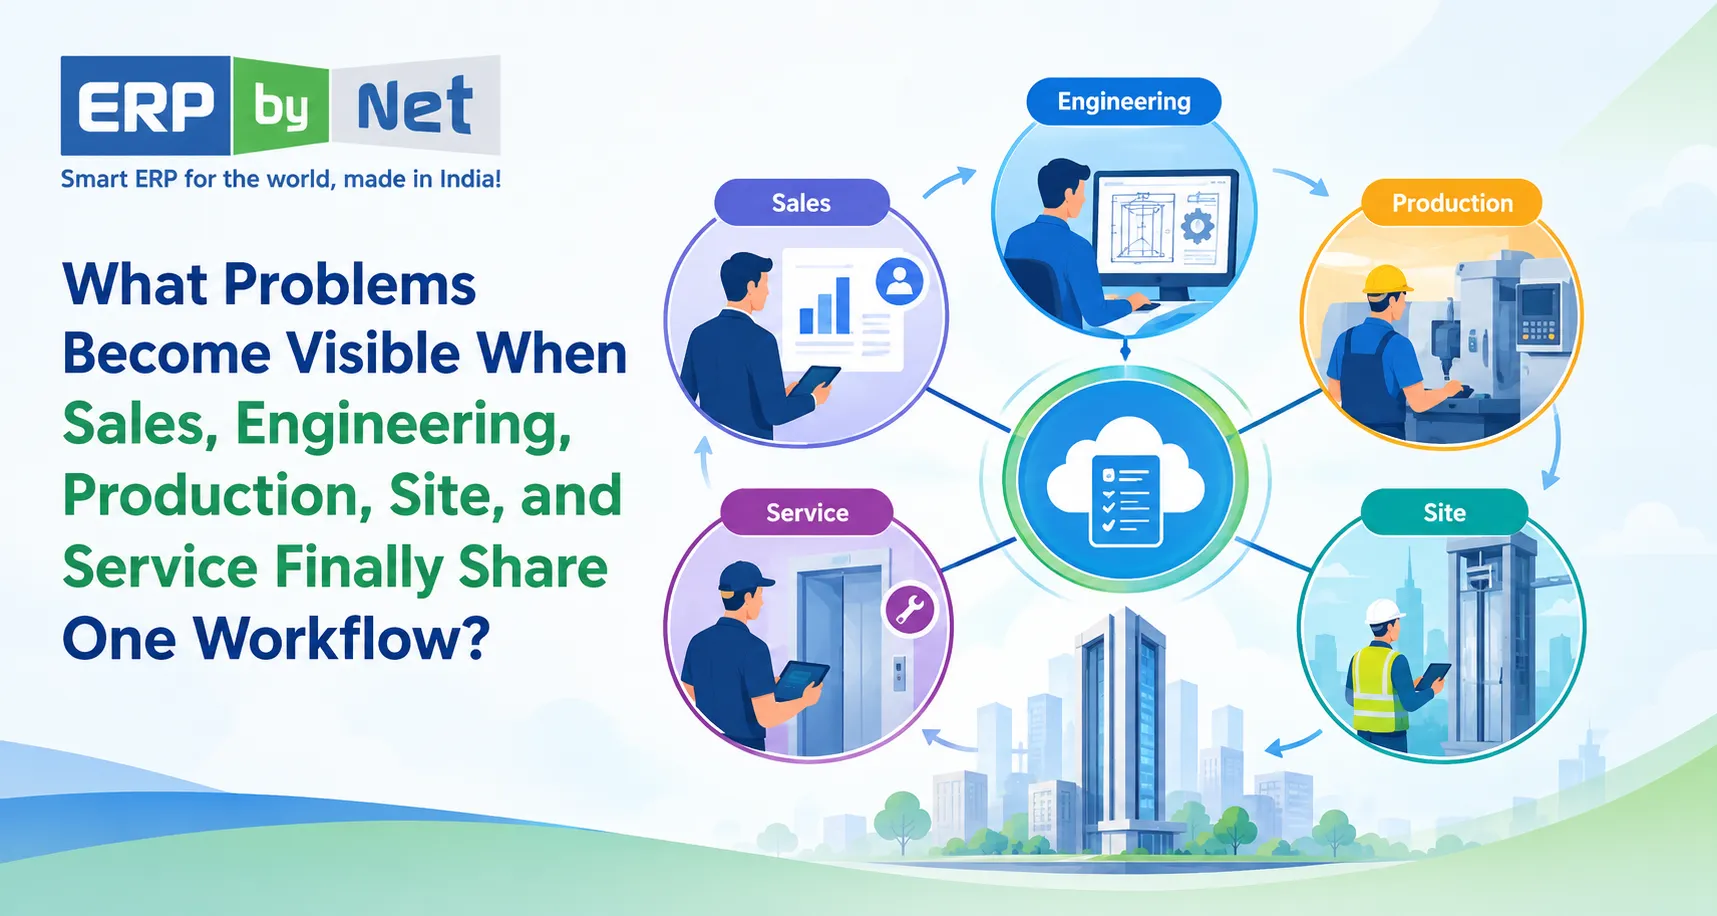
What Problems Become Visible When Sales, Engineering, Production, Site, and Service Finally Share One Workflow?

Key Takeaways

  • Disconnected departments create hidden process gaps even when each team manages its work correctly.
  • Engineering changes can affect materials, production, site work, and project costs.
  • Physical stock does not always mean available stock when materials are allocated, reserved, or incomplete.
  • Production completion does not always mean site readiness.
  • Connected ERP helps trace problems back to where they started, not just where they became visible.

What You’ll Learn

  • How connected workflows link sales, engineering, production, site, and service.
  • Why engineering changes need to reach downstream teams quickly.
  • How material planning and inventory visibility affect production readiness.
  • Why site readiness and production completion must be tracked separately.
  • How ERPbyNet connects the workflow from sales through finance and service.

Real Insights

  • The department where a problem appears is not always where it started.
  • A production delay may begin with an engineering change or material gap.
  • A site delay may come from an earlier planning or readiness issue.
  • A service complaint can reveal an earlier installation or configuration problem.
  • Connected information helps management move from “Where is the problem?” to “Where did it begin?”

A project can look healthy in one department and already be heading toward trouble somewhere else.

Sales may see a confirmed order. Engineering may still be working through specifications. Production may be waiting for material. The site team may be waiting for readiness confirmation. Service may later receive a complaint without having the complete history of what was installed.

Each department may be doing its job.

Yet the project can still be delayed, costs can increase, and customers can become dissatisfied.

The problem is often not that individual departments are incapable of managing their work. The problem is that the information connecting those departments is fragmented.

When sales, engineering, production, site, and service finally work through one connected workflow, something important changes.

The business does not simply gain visibility.

It starts seeing where problems actually enter the process.

For engineering, manufacturing, elevator, installation, and other project-based businesses, this distinction matters because a decision made at the beginning of an order can affect material planning, production, installation, project cost, and service months later.

A connected ERP workflow helps bring those relationships into view.

Why Department-Level Visibility Is Not Enough

Connected ERP workflow linking sales, engineering, production, site installation, and service for elevator project management

Imagine five teams managing the same project.

Sales knows what the customer ordered.

Engineering knows how it should be designed.

Production knows what needs to be manufactured.

Site knows what needs to be installed.

Service knows what needs to be maintained.

But if every team maintains its own information, the business can end up with five different versions of the same project.

A quotation may contain one specification.

A drawing may contain another.

A BOM may reflect a later revision.

Production may work from an older instruction.

The site team may not know which materials are expected.

Service may receive incomplete equipment information after handover.

This creates a dangerous situation:

Every department can have accurate information locally while the overall project information remains inconsistent.

That is where connected workflow becomes important.

ERPbyNet is designed around this type of operational environment, connecting sales, projects, manufacturing, inventory, service, technicians, and finance within an integrated ERP ecosystem.

What Changes When One Workflow Connects the Business?

A connected workflow creates a chain where information created at one stage becomes useful at the next.

Instead of managing isolated activities:

Sales → Engineering → Production → Site → Service

the business can create a connected operational flow:

Customer Requirement → Quote → Engineering → BOM/Material Planning → Production → Site Installation → Handover → Service

The important part is not the diagram itself.

The important part is the relationship between each stage.

A quotation can influence engineering.

Engineering can influence product configuration and material requirements.

Material planning can influence procurement and production readiness.

Production can influence site scheduling.

Site execution can influence project completion.

Installation data can become useful to service.

This is where hidden problems start becoming easier to identify.

1. Sales Commitments That Engineering Cannot Deliver as Planned

A sales team often has to respond quickly to customer expectations.

A quotation may be prepared based on:

  • Customer requirements
  • Product configuration
  • Technical specifications
  • Expected delivery date
  • Commercial assumptions
  • Project scope

But what happens after the order is confirmed?

If the information does not move cleanly into engineering, the engineering team may need to recreate or verify details manually.

That can introduce delays before production has even started.

The problem may not be in engineering

Suppose a customer changes:

  • Capacity
  • Dimensions
  • Finishing
  • Door configuration
  • Control requirements
  • Installation conditions
  • Optional components

If those changes remain inside emails, spreadsheets, or conversations, engineering may not have a reliable view of the latest requirement.

The project can then move forward with uncertainty.

A connected workflow helps make the transition from commercial requirement to technical definition more structured.

ERPbyNet’s SalesPundit supports CRM, quotations, tender workflows, pricing, sales approvals, and sales operations for engineering and project-based businesses. Its Product Definition Studio is designed for complex product configuration and technical rules, helping connect product definition with downstream requirements.

What becomes visible?

Instead of discovering the issue after production begins, the business can identify:

Customer requirement → Technical validation → Configuration → Engineering readiness

The earlier the mismatch appears, the earlier the business can respond.

2. Engineering Changes That Do Not Reach Production in Time

Engineering changes are normal in project-based manufacturing.

The problem begins when the change reaches one department but not another.

Consider a simple sequence:

Drawing Revision → BOM Change → Material Change → Production Change

If only the drawing changes, production may continue using an older BOM.

If the BOM changes but procurement has already placed an order, the business may suddenly have material that is no longer required.

If production discovers the change late, the result may be:

  • Rework
  • Material wastage
  • Production interruption
  • Additional procurement
  • Schedule changes
  • Cost increases

A connected workflow exposes the dependency

Engineering is not an isolated activity.

A technical change can create a commercial, material, production, site, and financial impact.

This is particularly important for Engineer-to-Order and configurable products where one customer order can generate different technical requirements.

ERPbyNet supports product definition, technical configuration, costing logic, engineering requirements, and drawing generation, while its material planning and production capabilities connect those requirements with downstream operations.

The objective is not simply to store the latest drawing.

It is to help ensure that the right information reaches the next stage of execution.

3. Production Delays That Actually Start in Material Planning

A production team may appear to have a productivity problem.

Machines are available.

Workers are available.

The production schedule exists.

Yet production is waiting.

Why?

Because one critical component is missing.

This is where disconnected workflows create misleading conclusions.

The visible problem is:

Production is delayed.

The actual problem could have started much earlier:

Customer order → Engineering → BOM → Material demand → Inventory → Procurement → Production

“We have stock” does not always mean “production can start”

Inventory may exist physically, but it may already be:

  • Allocated to another project
  • Reserved for another order
  • Located in another warehouse
  • Awaiting inspection
  • Incomplete as a required kit
  • Insufficient for the current requirement

This distinction becomes critical when multiple projects are running simultaneously.

ERPbyNet’s AceMRP connects material planning, inventory, procurement, warehouse operations, and manufacturing coordination. Its existing content also emphasizes that physical stock does not necessarily mean material is available for a particular requirement.

What becomes visible?

Instead of simply asking:

“Why is production late?”

management can begin asking:

“Which material requirement caused the production constraint, and where did that requirement originate?”

That is a much more useful question.

4. Procurement That Reacts Instead of Planning

Disconnected systems often make procurement highly reactive.

A purchase team receives a request.

They check availability.

They contact vendors.

They follow up on delivery.

Production follows up again.

Then another department asks for an updated status.

The cycle repeats.

The real challenge is not simply purchasing.

It is knowing:

  • What is required?
  • For which project?
  • In what quantity?
  • By when?
  • What is already available?
  • What is committed?
  • What is on order?
  • What has a long lead time?
  • What could become a production constraint?

ERPbyNet’s MRP capabilities are positioned around these connected planning requirements, including material demand, inventory, procurement, and production coordination.

The difference is timing

Good material planning is not only about knowing what to buy.

It is about knowing when the business needs it.

That changes procurement from:

“Something is missing. Purchase it.”

to:

“This requirement is expected to become a constraint. Plan it before it affects production.”

5. Production Completion Does Not Mean the Project Is Ready for Site

This is one of the most important problems in project-based businesses.

A factory may complete its production activities.

But the installation team may still be unable to proceed.

Why?

Because site execution depends on more than manufacturing completion.

It may depend on:

  • Site readiness
  • Material availability
  • Installation sequence
  • Civil work completion
  • Customer readiness
  • Required approvals
  • Manpower availability
  • Equipment movement
  • Project schedule

For an elevator project, for example, manufacturing completion does not automatically mean the shaft is ready for installation.

The hidden gap

A disconnected business may report:

Production: 100% complete

while the project remains:

Site: Not ready

Both statements can be correct.

But management needs to understand the relationship between them.

ERPbyNet’s AceSiteManager is designed to connect project implementation, site activities, installation, commissioning, contract dates, supply chain information, and project updates.

What becomes visible?

The business can start distinguishing between:

Production readiness

and

Installation readiness

That difference can prevent teams from assuming that a completed manufacturing stage automatically means the project can move forward.

6. Site Delays That Are Actually Caused by Earlier Decisions

When an installation team reaches a site and cannot proceed, the problem may appear to belong to the site team.

But consider what may have happened earlier.

The quotation may have missed a requirement.

Engineering may have changed a configuration.

Procurement may have delivered material late.

Production may have completed only part of the requirement.

The customer may not have completed site preparation.

The site team may therefore become the final point where an earlier problem becomes visible.

This creates an important principle:

The department where a problem becomes visible is not always the department where the problem began.

A connected workflow makes those dependencies easier to trace.

7. Installation Data That Gets Lost Before Service Starts

The project does not end when installation is completed.

For many businesses, installation is the beginning of a long service relationship.

This is especially important for elevator and equipment businesses where the installed product may require:

  • Preventive maintenance
  • Breakdown service
  • Inspections
  • Spare parts
  • Warranty support
  • AMC management
  • Technician visits
  • Contract renewals

If service teams receive incomplete installation information, they may have to ask questions that should already have answers.

What was installed?

Which configuration?

Which components?

When was it commissioned?

What warranty applies?

What service contract is active?

What work has already been performed?

The project history should not disappear at handover

A connected workflow allows information created during sales, engineering, production, and installation to remain useful after the project moves into service.

ERPbyNet’s AceService supports preventive maintenance scheduling, callback ticket management, contract renewals, technician tracking, and service updates. MyAceService and SmartTechnician extend service operations into mobile workflows.

The goal is simple:

Installation information should become service information instead of becoming history that nobody can easily access.

8. Service Complaints That Reveal Earlier Process Gaps

A service complaint is usually treated as a service issue.

But sometimes the complaint is a symptom of an earlier operational problem.

For example:

Repeated service issue

→ Incorrect component selection

→ Engineering/configuration issue

→ Procurement or production substitution

→ Installation variation

→ Service problem

Without connected information, the service team may only see the final complaint.

With a connected workflow, the business has a better opportunity to investigate the history behind it.

From ticket handling to root-cause visibility

Service data can become more useful when it is connected to the equipment, project, installation history, and customer information.

That can help businesses move beyond:

“Close the ticket.”

toward:

“Why is this issue happening repeatedly?”

That distinction matters for both service quality and operating cost.

9. Project Cost Overruns That Appear Too Late

A project may start with a planned cost.

But costs can change throughout execution.

Consider what can affect project profitability:

  • Additional material
  • Engineering changes
  • Rework
  • Subcontracting
  • Additional site visits
  • Installation delays
  • Logistics
  • Overtime
  • Service callbacks
  • Unplanned expenses

If finance only sees the final numbers after the project is completed, management may learn about the margin problem too late.

Profitability needs operational context

A project cost figure becomes much more useful when it can be related to the activities that created it.

For example:

Material variance

→ Engineering change

Labour variance

→ Installation delay

Subcontracting cost

→ Site execution issue

Additional service cost

→ Repeated equipment problem

ERPbyNet connects operational processes with finance and project-related information, including budgeting, cost allocation, AP/AR, and financial reporting.

The objective is not simply to report that a project exceeded its budget.

It is to help management understand where the project started moving away from the original plan.

10. Management Follow-Ups That Reveal a Lack of System Visibility

One of the most overlooked symptoms of disconnected operations is the number of questions management has to ask manually.

“What’s the status?”

“Has engineering approved it?”

“Is the material available?”

“Why hasn’t production started?”

“Is the site ready?”

“Has the installation been completed?”

“Is the AMC active?”

“Why is this project over budget?”

If employees have to manually collect answers from different departments every time management asks a question, the business has an information-flow problem.

A connected workflow changes the conversation

Instead of spending time collecting information, management can focus more on exceptions:

  • Which projects are behind schedule?
  • Which material shortages can affect production?
  • Which sites are not ready?
  • Which projects are exceeding budget?
  • Which service contracts require attention?
  • Which orders have unresolved engineering changes?

ERPbyNet provides centralized reporting and user-defined reporting capabilities across its operational environment, supporting visibility across complex business processes.

What Does One Connected Workflow Actually Connect?

A useful ERP workflow is not simply a collection of software modules.

It is the relationship between business events.

The connected chain can look like this:

Sales

Customer requirement, quotation, pricing, approvals

↓

Engineering

Product configuration, technical rules, drawings, BOM

↓

Material Planning

Demand calculation, inventory availability, procurement requirements

↓

Production

Scheduling, work centers, manufacturing execution

↓

Site

Material movement, installation activities, project progress, commissioning

↓

Service

Maintenance, callbacks, technician visits, AMC and warranty

↓

Finance

Costs, budgets, receivables, payables, profitability

The value comes from the information moving between these stages.

ERPbyNet’s platform is positioned around connecting sales, projects, manufacturing, inventory, service, technicians, and finance for operationally complex businesses.

Read More: How Can ERPbyNet Help Management Move From Reactive Problem-Solving to Proactive Control?

How ERPbyNet Helps Turn These Gaps Into a Connected Workflow

ERP workflow connecting sales, engineering, material planning, production, site installation, service, and finance for elevator projects

ERPbyNet is built for businesses where operations do not stop at manufacturing or sales.

Its positioning specifically covers elevator companies, engineering businesses, manufacturing organizations, project-based companies, and service and maintenance operations.

Sales to Engineering

SalesPundit supports CRM, quotations, tender workflows, pricing, approvals, and sales operations.

For complex products, Product Definition Studio supports product configuration, technical rules, specifications, and costing logic.

This creates a stronger bridge between what was sold and what needs to be engineered.

Engineering to Material Planning

Engineering requirements can influence BOMs and material demand.

AceMRP provides material planning, inventory, procurement, warehouse, and manufacturing coordination.

This helps connect technical requirements with material decisions instead of treating them as separate activities.

Material Planning to Production

Production needs more than a schedule.

It needs the required material, appropriate planning, and visibility into what can become a constraint.

ERPbyNet connects MRP and production workflows to help create this operational relationship.

Production to Site

AceSiteManager supports project implementation, installation activities, scheduling, budgets, site operations, and project reporting.

This helps connect factory-side progress with what is happening at the installation site.

Site to Service

Once installation and commissioning are completed, the operational relationship can continue into service.

AceService, MyAceService, and SmartTechnician support service contracts, maintenance, callback tickets, technician activities, field updates, and service coordination.

Operations to Finance

The final objective is not just operational visibility.

The business also needs to understand the financial impact of those operations.

ERPbyNet’s finance capabilities support areas such as AP/AR, budgeting, cost allocation, GST reporting, assets, and financial operations.

The Real Value of Connecting the Workflow

A connected workflow does not mean that every problem disappears.

It means the business has a better way to see the relationship between problems.

A delayed project may be connected to a material shortage.

The material shortage may be connected to an engineering change.

The engineering change may have originated from a customer requirement.

The additional cost may later appear in project profitability.

A service complaint may eventually reveal an installation or product configuration issue.

These relationships are difficult to see when every department works from isolated information.

They become easier to investigate when the workflow is connected.

From “Where Is the Problem?” to “Where Did the Problem Begin?”

This is perhaps the biggest shift.

In a disconnected environment, management often asks:

“Which department is causing the delay?”

In a connected environment, a better question becomes:

“At which stage did the process start moving away from plan?”

That difference matters.

Because the department reporting the problem may simply be the department that encountered the consequence.

The original cause may have entered the workflow much earlier.

Why This Matters for Elevator and Engineering Businesses

For elevator companies and engineering organizations, the workflow is particularly interconnected.

A typical project can involve:

Customer Requirement

→ Site Survey

→ Quotation

→ Product Configuration

→ Engineering

→ BOM

→ MRP

→ Procurement

→ Production

→ Material Movement

→ Installation

→ Commissioning

→ AMC

→ Service

A change at the beginning can influence several downstream activities.

ERPbyNet specifically positions its elevator ERP capabilities around quotations, site surveys, manufacturing, installation, AMC, technician management, service requests, inventory, procurement, and finance.

That makes workflow connectivity particularly relevant where every project has its own configuration, schedule, material requirements, site conditions, and service history.

What a Connected ERP Workflow Should Help You Ask

Instead of simply asking whether every department is using ERP, ask whether information is actually moving between them.

Ask:

Can sales see what engineering has approved?

Can engineering changes influence material requirements?

Can production see material constraints before the schedule is affected?

Can procurement see what is required and when it is required?

Can site teams see what is expected to arrive and what must happen next?

Can management connect project progress with project cost?

Can service teams access the history created before handover?

Can the business trace a visible problem back to the stage where it started?

These questions reveal whether an ERP is functioning as a connected operating system or simply as a collection of departmental tools.

A Connected Workflow Is More Than “One Software”

The real objective is not to put every department on the same screen.

It is to make information useful beyond the department that created it.

A sales quotation should become useful to engineering.

Engineering should become useful to MRP.

MRP should become useful to procurement and production.

Production should become useful to project execution.

Site execution should become useful to service.

Service history should become useful to management and finance.

That is what creates continuity.

The workflow becomes one chain instead of a series of handoffs.

Read More: What Features Should an MRP System Have for Complex Elevator Manufacturing?

ERPbyNet
Connect Every Stage. Expose the Gaps.
ERPbyNet connects sales, engineering, production, site, service, and finance in one workflow—helping teams identify delays, rework, material gaps, missed handoffs, and cost issues earlier.
Connected ERP • Sales to Service
Bring disconnected processes together with ERPbyNet.

Turn Connected Information Into Better Decisions

When Sales, Engineering, Production, Site, and Service work from one connected workflow, problems become easier to trace before they turn into delays, rework, cost overruns, or customer issues. A production delay can reveal a material gap, a site delay can point to readiness issues, and a service complaint can uncover an earlier installation or configuration problem.

ERPbyNet connects these critical stages with Sales, Engineering, Material Planning, Production, Site, Service, and Finance working within one connected ERP environment.

The goal is simple: don’t just know where a problem appears—understand where it started.

With connected information flowing across every stage, your teams can respond earlier, coordinate better, and keep projects moving with greater control.

Connect your workflow. Expose hidden gaps. Keep your business moving.

Frequently Asked Questions

What is a connected ERP workflow?

A connected ERP workflow links business activities so information created in one process can support the next process. For project-based and engineering businesses, this can connect sales, engineering, material planning, procurement, production, site execution, service, and finance.

Why is connecting sales and engineering important?

Sales captures customer requirements and commercial commitments, while engineering translates those requirements into technical specifications. Connecting the two can reduce repeated data entry and help identify requirement or configuration gaps earlier.

How does ERP connect engineering with production?

Engineering information can influence product definitions, BOMs, material requirements, and production planning. A connected ERP environment helps these downstream processes work from related information instead of requiring teams to recreate it manually.

Can ERP help identify the cause of production delays?

ERP cannot automatically eliminate every production delay, but connected information can make contributing factors easier to identify. Material shortages, procurement delays, engineering changes, planning constraints, and other dependencies can be investigated as part of the same workflow.

Why is site management important in project-based ERP?

Production completion does not necessarily mean a project is ready for installation. Site readiness, material availability, schedules, manpower, customer dependencies, and installation activities all influence project execution. ERPbyNet’s AceSiteManager is designed to connect these site activities with project and supply-chain information.

How does ERP connect installation with service?

Installation creates important information about the equipment, project, configuration, commissioning, and handover. When that information remains connected to service operations, service teams can work with greater access to the history of the installed equipment.

Is ERPbyNet suitable for elevator companies?

ERPbyNet is specifically positioned for elevator manufacturers, installation companies, modernization contractors, and service providers, with capabilities covering quotations, site surveys, manufacturing, installation, AMC, service, technicians, inventory, procurement, and finance.

Is ERPbyNet suitable for engineering and project-based businesses?

Yes. ERPbyNet positions its platform for engineering companies, manufacturing businesses, project-based organizations, and service and maintenance businesses that require coordination across sales, engineering, projects, inventory, production, site execution, service, and finance.

What makes a connected ERP workflow different from separate software systems?

Separate systems can manage individual departmental activities, but information may still need to be transferred manually between them. A connected ERP workflow is designed around the relationships between those activities so information can continue through the business process instead of stopping at departmental boundaries.

CategoriesERP (Enterprise Resource Planning) ERP Solutions

How Can ERPbyNet Help Management Move From Reactive Problem-Solving to Proactive Control?

Key Takeaways

  • Reactive management starts when problems are found too late, leaving teams with limited time to respond.
  • Disconnected data creates operational blind spots across projects, inventory, service, and procurement.
  • Real-time ERP visibility helps identify risks early and supports faster decisions.
  • Automated alerts and workflows reduce manual follow-ups and improve operational control.
  • ERP helps businesses move from firefighting to proactive management by making problems visible before they become critical.

What You’ll Learn

  • Why businesses become reactive as operations grow more complex.
  • How real-time ERP visibility improves operational control.
  • How early alerts and automated workflows help prevent delays.
  • Why connected data across departments improves decision-making.
  • How ERPbyNet helps management shift from reactive problem-solving to proactive control.

Real Insights

  • Most operational problems become expensive when detected late.
  • Manual reports often show what already happened instead of what needs attention next.
  • Real-time visibility helps teams spot shortages, delays, and bottlenecks early.
  • Proactive management depends on connected information, not more manual reporting.
  • The goal of ERP is not just to record problems but to help management act before they escalate.

Management becomes difficult when problems are discovered only after they have already affected operations.

A material shortage is noticed when production is about to stop. A project delay becomes visible when the deadline is already at risk. A customer complaint remains unresolved because nobody has a clear view of its status. A service contract approaches expiry without timely follow-up. Management then has to step in, investigate what went wrong, coordinate different teams, and find a solution under pressure.

This is reactive management.

Modern businesses need a different approach: identifying risks earlier, monitoring operations continuously, and taking action before small issues become expensive problems.

This is where an integrated ERP system can make a significant difference.

ERPbyNet connects sales, projects, manufacturing, inventory, procurement, service, field technicians, finance, and reporting within one integrated ERP ecosystem. This gives management a more complete view of business operations and helps teams move from manual follow-ups and delayed reporting toward real-time visibility, structured workflows, and proactive decision-making.

What Is the Difference Between Reactive and Proactive Management?

Reactive management focuses on solving problems after they occur.

The process often looks like this:

Problem occurs → Someone notices it → Management investigates → Teams coordinate → Corrective action is taken

For example, if a production team discovers that a critical component is unavailable, the procurement team may need to urgently contact suppliers, check alternative sources, update production schedules, and inform management.

The problem is being solved, but the organization is spending time and money responding to something that could potentially have been identified earlier.

Proactive management changes the process:

Business data → Early signal → Management insight → Planned action → Controlled outcome

Instead of waiting for the material shortage, managers can monitor inventory and material requirements, identify potential shortages, and take action earlier.

Instead of discovering a project delay after a milestone is missed, management can monitor project progress and identify deviations while there is still time to correct them.

This is the fundamental shift ERP can enable.

Read More: What Is Really Behind Cost Overruns in Elevator Projects-and How Can ERP Help Control Them?

Why Businesses Struggle With Reactive Problem-Solving

ERPbyNet connects business functions to reduce reactive problem-solving

Many businesses do not intentionally choose reactive management. It develops because information is fragmented.

Different departments may use:

  • Spreadsheets
  • Emails
  • WhatsApp messages
  • Separate software systems
  • Manual reports
  • Phone calls
  • Paper-based records

The result is that management often receives information after it has already passed through several people and systems.

A project manager may know that a site is delayed, while procurement does not know that the delay is related to material availability. Finance may not immediately see the cost impact. Senior management may only discover the issue during a weekly or monthly review.

When information is disconnected, management becomes dependent on follow-ups instead of visibility.

ERPbyNet addresses this problem by bringing key business functions into one connected platform, including sales, project execution, manufacturing, inventory, service, technician operations, and finance.

How ERPbyNet Helps Management Move Toward Proactive Control

1. Real-Time Visibility Helps Management See Problems Earlier

One of the biggest differences between reactive and proactive management is when the problem becomes visible.

If management receives information only through periodic reports, decisions are naturally based on historical information.

Real-time visibility changes that.

ERPbyNet provides centralized visibility across important operational areas, helping management monitor activities such as:

  • Project progress
  • Inventory levels
  • Material requirements
  • Manufacturing operations
  • Service requests
  • Technician activities
  • Maintenance schedules
  • Financial information
  • Sales activities
  • Operational reports

ERPbyNet’s platform is designed to connect departments and provide visibility across complex operational environments rather than forcing managers to collect updates from multiple systems.

This creates a simple but important advantage:

Managers can spend less time asking what is happening and more time deciding what should happen next.


2. Integrated Data Creates a Single Source of Operational Truth

Proactive management depends on reliable information.

If sales, inventory, production, projects, and finance each have different versions of business data, management cannot easily understand the complete situation.

For example, suppose a large customer order enters the business.

Management may need to know:

  • Is the required material available?
  • Can production meet the required quantity?
  • Is additional procurement required?
  • Does the production schedule have sufficient capacity?
  • Will the order affect existing projects?
  • What will be the financial impact?
  • Can the delivery timeline be achieved?

When these functions operate independently, answering these questions requires coordination between multiple teams.

An integrated ERP environment connects the information.

ERPbyNet brings sales, engineering, projects, manufacturing, inventory, service, and finance into a connected operational environment.

This helps management make decisions using a broader picture rather than isolated departmental information.

3. ERPbyNet Helps Identify Material and Inventory Risks Before They Become Disruptions

Inventory problems are one of the clearest examples of reactive management.

Without accurate visibility, businesses may discover material shortages only when production or project execution is affected.

ERPbyNet includes material planning, inventory management, warehouse operations, procurement workflows, and manufacturing coordination through its MRP capabilities.

This enables management to monitor material requirements and inventory conditions more effectively.

For example:

Reactive approach

Material shortage → Production affected → Emergency procurement → Delivery delay

Proactive approach

Material requirement identified → Inventory checked → Procurement planned → Material available when required

The goal is not simply to maintain more inventory.

The goal is to have better information about what is required, what is available, and what needs attention.

ERPbyNet’s MRP functionality is designed to support this type of planning and coordination.

4. Project Visibility Helps Management Control Delays Before They Escalate

Project-based businesses face another major challenge: delays can develop gradually.

A project may appear to be progressing normally while small issues accumulate:

  • A material delivery is late.
  • A site activity is incomplete.
  • A technician is unavailable.
  • A milestone is delayed.
  • Labour productivity is lower than expected.
  • A project cost starts moving away from the planned budget.

If management only reviews the project after a milestone is missed, the available time to correct the situation is already limited.

ERPbyNet’s project and site management capabilities provide visibility into project schedules, execution activities, workforce activities, budgets, and site operations.

This allows managers to monitor project execution more closely and intervene when something begins moving away from plan.

The objective is simple:

Don’t wait for the deadline to reveal the problem. Monitor the process that leads to the deadline.

5. Automated Workflows Reduce Dependence on Manual Follow-Ups

Manual follow-ups are another major reason management becomes reactive.

A manager may have to ask:

“Has this approval been completed?”

“Did procurement place the order?”

“Has the technician visited the site?”

“Why is this complaint still pending?”

“Who is responsible for this task?”

When these questions must be answered manually, management spends valuable time chasing information.

ERPbyNet supports configurable workflows, approval systems, and business processes that can reduce manual coordination.

For example, workflows can help structure:

Request → Approval → Assignment → Execution → Update → Completion

This creates greater process discipline and makes responsibilities clearer.

Automation does not eliminate management involvement. Instead, it helps managers focus their attention on exceptions and decisions that actually require management intervention.

6. Service Management Can Shift From Reactive Repairs to Preventive Action

Service businesses often operate reactively.

A customer reports a problem.

Then the business:

  1. Receives the complaint
  2. Assigns a technician
  3. Checks availability
  4. Arranges spare parts
  5. Schedules the visit
  6. Resolves the issue

While reactive service will always be necessary, businesses can reduce avoidable emergencies by using preventive maintenance and service planning.

ERPbyNet’s AceService capabilities support preventive maintenance scheduling, callback ticket management, technician tracking, contract renewals, and service updates.

This allows businesses to manage service operations before every issue becomes an emergency.

For example, instead of waiting for an equipment problem:

Maintenance due → Schedule service → Assign technician → Complete maintenance → Record service history

This creates a more controlled service environment and can improve customer experience.

7. Technician and Field Visibility Gives Management Control Beyond the Office

For businesses with technicians, installation teams, or field employees, office-based management can create a significant visibility gap.

Management may know that a task was assigned but not know:

  • Whether the technician reached the site
  • What work has been completed
  • What issue was found
  • Whether additional material is required
  • Whether the job is still pending
  • How long the activity is taking

ERPbyNet supports mobile applications such as SmartTechnician, MyAceService, and SiteApp to connect field activities with broader business processes. SmartTechnician supports capabilities including GPS-based tracking, route management, ticket updates, check-ins, maintenance reporting, and field communication.

This helps reduce the gap between what management thinks is happening and what is actually happening in the field.

That difference is critical for proactive control.

8. Financial Visibility Helps Management Detect Cost Problems Earlier

Operational problems eventually become financial problems.

A project delay can increase labour costs.

A material shortage can increase procurement costs.

Poor inventory planning can lock working capital into unnecessary stock.

Service inefficiencies can reduce profitability.

If finance information is separated from operational information, management may see the financial impact only after the damage has already occurred.

ERPbyNet’s AceFinance module supports areas including accounts payable and receivable, GST reporting, budgeting, asset tracking, cost allocation, and financial operations.

When financial and operational information are connected, management can better understand the relationship between:

Operational activity → Resource usage → Cost → Profitability

This makes financial control part of day-to-day management rather than something reviewed only after the reporting period.

9. Dashboards and Reports Turn Business Data Into Management Insights

Having data is not the same as having useful information.

A business may have thousands of records, but management needs answers to specific questions:

  • Which projects are at risk?
  • Which materials require attention?
  • Which service requests are pending?
  • Which customers require follow-up?
  • Where are operational bottlenecks developing?
  • Which activities are affecting costs?
  • Which teams require additional support?

ERPbyNet supports user-defined reporting and business intelligence reporting across its modules.

This helps management move from simply collecting data to using data for decision-making.

The broader shift is:

Data → Information → Insight → Decision → Action

That is the foundation of proactive management.

10. ERPbyNet Helps Management Focus on Exceptions Instead of Monitoring Everything

Proactive control does not mean that managers need to monitor every transaction every minute.

That would simply replace manual work with another form of information overload.

The better approach is to allow the ERP system to handle routine transactions and provide management with visibility into areas that require attention.

For example:

Normal activity: Continue automatically through the defined workflow.

Exception: Flag the issue for review.

This allows managers to focus on questions such as:

  • Why is this project behind schedule?
  • Why is this material requirement still pending?
  • Why has this service request exceeded the expected timeline?
  • Why is this cost higher than planned?
  • Why has this approval remained incomplete?

This is where ERP moves beyond being a record-keeping system and becomes a management control system.

Read More : Why Modern AMC Management Needs More Than Renewal Reminders

Reactive vs Proactive Management With ERPbyNet

Reactive ManagementProactive Management with ERPbyNet
Problems are discovered lateOperational signals are visible earlier
Managers depend on manual updatesManagers access centralized information
Departments work in silosProcesses are connected across departments
Inventory shortages cause emergenciesMaterial requirements can be planned
Project delays are discovered lateProject execution can be monitored continuously
Service starts after complaintsPreventive maintenance can be scheduled
Field teams are difficult to monitorMobile field visibility improves coordination
Reports explain what already happenedData supports faster decisions and action
Managers spend time chasing updatesManagers can focus on exceptions and priorities


Why This Matters for Engineering, Manufacturing, Elevator, and Project-Based Businesses

The shift from reactive to proactive control is particularly important for businesses where operations depend on multiple interconnected activities.

For example, an engineering or elevator company may need to coordinate:

Sales → Engineering → Procurement → Inventory → Manufacturing → Project Execution → Installation → Service → Finance

A delay at one stage can affect multiple downstream activities.

ERPbyNet is specifically positioned for elevator companies, engineering businesses, manufacturers, project-based organizations, and service and maintenance businesses. Its platform connects these operational areas to improve coordination and visibility.

That makes proactive control especially valuable.

Instead of managing each department independently, management can look at the complete operational chain.

What Does the Shift From Reactive to Proactive Actually Look Like?

Consider a simple example.

A company is executing an engineering project.

Without integrated ERP

The project manager discovers that a required component is missing.

They contact procurement.

Procurement checks the supplier.

The supplier says delivery will be delayed.

The project manager informs management.

Management asks finance about the additional cost.

Finance requests project information.

Several calls and messages later, everyone understands the situation.

By then, the project schedule may already be affected.

With an integrated ERP approach

The material requirement is connected to project planning.

Inventory availability can be checked.

Procurement requirements can be identified.

Project progress is visible.

Management can review the operational situation through centralized information.

The objective is not that ERP magically prevents every problem.

The objective is that the organization becomes aware of important problems earlier and has better information for deciding what to do next.

That is what proactive control really means.

ERPbyNet Is More Than an ERP System for Recording Transactions

A modern ERP should not only answer:

“What happened?”

It should help management answer:

“What is happening now?”

and increasingly:

“What needs attention next?”

ERPbyNet brings operational functions together through modules and applications covering sales, projects, manufacturing, inventory, service, field operations, finance, reporting, and more.

This integrated approach helps create a foundation for:

  • Real-time operational visibility
  • Better planning
  • Faster decision-making
  • Workflow automation
  • Improved accountability
  • Better cross-functional coordination
  • Earlier identification of operational risks
  • Stronger project and service control

The result is a management environment where decisions can be based on current operational information rather than delayed updates.

How to Start Moving From Reactive to Proactive Management

Six-step business management roadmap showing how companies move from reactive problem-solving to proactive management

Businesses do not need to transform every process overnight.

A practical approach is to start with the areas where reactive problem-solving creates the greatest cost or operational risk.

Step 1: Identify Repeated Problems

Look for issues that management repeatedly has to solve:

  • Material shortages
  • Project delays
  • Service complaints
  • Approval delays
  • Inventory mismatches
  • Technician coordination
  • Cost overruns

Step 2: Identify Where Information Gets Delayed

Ask:

Where does management currently have to call, message, or email someone to get an operational update?

These are potential visibility gaps.

Step 3: Connect the Relevant Processes

Instead of managing sales, inventory, projects, service, and finance separately, connect the workflows that influence each other.

Step 4: Automate Routine Processes

Approvals, task assignments, notifications, reporting, and recurring processes can be structured through workflows.

Step 5: Build Management Visibility

Create reports and dashboards around the metrics that actually influence decisions.

Step 6: Manage Exceptions

Once routine operations are structured, management can focus more attention on delays, risks, exceptions, and opportunities.

This is how an organization gradually moves from firefighting to control.

The Business Value of Proactive ERP Management

Moving from reactive to proactive management is not simply about adopting new software.

It changes how the organization operates.

Instead of spending management time on:

“Why did this happen?”

teams can increasingly focus on:

“What should we do next?”

That shift can help businesses improve:

Operational Efficiency

Connected workflows reduce unnecessary manual coordination and information chasing.

Decision-Making

Management gets access to more current and connected operational information.

Project Control

Project progress, activities, resources, and budgets can be monitored more systematically.

Inventory Planning

Material requirements and inventory information can support better procurement and production planning.

Service Performance

Preventive maintenance, technician coordination, service requests, and contracts can be managed through structured processes.

Financial Control

Operational activity can be connected with financial information to improve cost and profitability visibility.

Scalability

Standardized and connected processes make it easier to manage increasing operational complexity.

Why ERPbyNet Can Be a Strong Foundation for Proactive Business Management

The goal of ERP implementation should not simply be to replace spreadsheets with another software system.

The bigger objective is to create a connected operating environment where information flows between departments and management can make decisions with greater visibility.

ERPbyNet is built around this approach.

Its ecosystem connects sales, engineering, projects, manufacturing, inventory, service, field operations, and finance while also providing mobile applications for technicians and site teams.

For businesses dealing with complex projects, manufacturing requirements, field teams, service operations, or elevator and engineering workflows, this connected structure can help reduce the information gaps that often lead to reactive decision-making.

The result is a gradual shift:

From disconnected data → connected information

From delayed reports → real-time visibility

From manual follow-ups → structured workflows

From reacting to problems → identifying risks earlier

From operational firefighting → proactive control

ERPbyNet
Move from Reactive Decisions to Proactive Control
ERPbyNet gives management connected visibility across projects, materials, service, operations, and finance—helping teams spot issues earlier and act before they become costly problems.
ERP • Real-Time Visibility • Proactive Control
Make better decisions with connected business visibility.

Final Thoughts

Reactive problem-solving will always be part of business management. Unexpected customer requirements, supply disruptions, equipment failures, and operational challenges cannot be completely eliminated.

The difference is how quickly a business can see, understand, and respond to those challenges.

An integrated ERP platform such as ERPbyNet can help management create that visibility by connecting business processes, centralizing operational information, automating workflows, supporting project and inventory planning, monitoring service and field activities, and connecting operational data with financial management.

For engineering, manufacturing, elevator, project-based, and service businesses, this can be particularly valuable because operations are rarely isolated. Sales decisions can affect procurement. Material availability can affect projects. Project delays can affect finance. Service performance can affect customer relationships.

When these processes are connected, management gets a clearer view of how one decision affects the rest of the business.

That is the real move from reactive problem-solving to proactive control:

Don’t wait for the problem to become visible. Build the visibility that helps your team act earlier.

If your business is still depending heavily on spreadsheets, manual reporting, disconnected applications, and constant management follow-ups, ERPbyNet can help you explore a more connected approach to operational management.

Want to see how ERPbyNet can fit your business processes? Talk to the ERPbyNet team to explore the right ERP modules and workflows for your organization.

FAQs

What does proactive management mean in ERP?

Proactive management means using connected business data, real-time visibility, workflows, reports, and planning tools to identify potential issues earlier and take action before they become larger operational problems.

How does ERP help managers make proactive decisions?

ERP centralizes business information across departments, giving managers better visibility into current operations. This can help them identify delays, inventory risks, project issues, service requirements, and financial concerns earlier.

How does ERPbyNet support proactive management?

ERPbyNet connects sales, projects, manufacturing, inventory, service, field operations, and finance. It also supports workflows, reporting, mobile field applications, project visibility, inventory planning, service management, and financial operations.

Can ERPbyNet help prevent inventory shortages?

ERPbyNet includes MRP, inventory management, warehouse operations, procurement workflows, and material planning capabilities. These help businesses monitor material requirements and make more informed procurement and production decisions.

How can ERPbyNet help with project delays?

ERPbyNet supports project and site management with visibility into schedules, execution activities, workforce activities, budgets, and site operations. This gives management better information for monitoring project progress and addressing issues earlier.

Can ERPbyNet support preventive maintenance?

Yes. ERPbyNet’s AceService capabilities include preventive maintenance scheduling, callback ticket management, technician tracking, contract renewals, and service updates.

Is ERPbyNet suitable for engineering and manufacturing companies?

Yes. ERPbyNet is designed for operationally complex businesses, including engineering companies, manufacturing businesses, elevator companies, project-based organizations, and service and maintenance businesses.

What is the biggest difference between reactive and proactive ERP management?

Reactive management focuses on solving problems after they occur. Proactive ERP management focuses on creating visibility, identifying risks earlier, planning actions, and managing exceptions before they become larger problems.

CategoriesElevator Maintenance Management ERP (Enterprise Resource Planning)

What Is Really Behind Cost Overruns in Elevator Projects-and How Can ERP Help Control Them?

Key Takeaways

  • Elevator project overruns build through small cost gaps across quotation, engineering, procurement, and installation.
  • Inaccurate BOMs and late engineering changes can increase material costs and cause rework.
  • Emergency procurement and installation delays can quickly reduce project margins.
  • Customer changes need cost visibility to prevent unbilled work from reducing profitability.
  • ERP helps track planned vs. actual costs so teams can act before overruns grow.

What You’ll Learn

  • Where cost overruns begin in elevator projects.
  • How BOM errors and engineering changes affect project costs.
  • Why material shortages and emergency purchases increase expenses.
  • How site delays, rework, and customer changes impact project margins.
  • How ERPbyNet helps monitor project costs from quotation to completion.

Real Insights

  • A project can stay on schedule and still lose money when costs are not tracked during execution.
  • One missing component can create multiple costs through urgent buying, idle labour, and extra site visits.
  • Project delays are cost events because they can increase labour, travel, and site expenses.
  • Planned vs. actual cost tracking exposes margin loss early instead of after project completion.
  • Cost control starts with visibility across every stage of the elevator project.

An elevator project can be completed on time, installed successfully, and handed over to the customer—and still deliver a disappointing financial result.

The reason is simple: project cost overruns rarely come from one dramatic mistake.

They often build gradually through small decisions and operational gaps:

  • An assumption made during quotation
  • A specification changed during engineering
  • A BOM that was not updated
  • Material purchased at the last minute
  • A supplier delivery that missed the required date
  • A customer change executed without proper cost visibility
  • Additional site visits
  • Idle installation manpower
  • Rework caused by incorrect information
  • Expenses that were recorded too late

Individually, these may look manageable.

Together, they can significantly reduce the margin of an elevator project.

This is particularly important because elevator projects are highly interconnected. Sales commitments influence engineering. Engineering determines the BOM. The BOM drives material planning and procurement. Material availability affects production and installation. Site conditions influence execution. And every delay or change can eventually affect project cost.

Research into project delays and overruns consistently identifies factors such as design changes, material shortages, supplier delays, poor coordination, scope changes and planning problems as contributors to cost and schedule performance.

So the real question is not simply:

“How can elevator companies reduce project costs?”

It is:

“How can elevator companies identify where project costs are beginning to move away from the original plan—while there is still time to act?”

That is where ERP can play a much more important role than simply automating transactions.

Why Elevator Projects Are Particularly Vulnerable to Cost Overruns

Elevator manufacturing and installation are not simple repetitive production activities.

Each project can involve different:

  • Building dimensions
  • Number of floors and stops
  • Load capacities
  • Cabin specifications
  • Door configurations
  • Drive and controller requirements
  • Safety requirements
  • Architectural requirements
  • Customer preferences
  • Site conditions
  • Installation constraints

The result is a project environment where one change can affect several departments simultaneously.

Consider a simplified workflow:

Sales → Quotation → Engineering → BOM → Material Planning → Procurement → Production → Site → Installation → Handover

The problem begins when these stages are managed as separate activities rather than connected processes.

A sales team may have one version of the customer requirement.

Engineering may work from another.

Procurement may purchase against an older BOM.

The production team may discover a missing component later.

The installation team may arrive before the site is ready.

Finance may eventually see the additional expenses—but only after they have already occurred.

This creates a dangerous situation:

The project is progressing operationally, but its financial performance is becoming less visible.

The Real Cost Overrun Often Starts Before Installation

Elevator project cost overrun caused by inaccurate quotation assumptions across equipment, materials, installation, site requirements, delivery, subcontracting, transportation, and engineering

One of the biggest misconceptions about project overruns is that they begin at the installation site.

Often, they begin much earlier.

Recent elevator modernization guidance similarly points to planning, scope review and contract development as areas where problems can originate before work reaches the field.

An elevator company may quote a project based on assumptions about:

  • Equipment requirements
  • Material quantities
  • Installation effort
  • Site readiness
  • Customer specifications
  • Delivery timelines
  • Subcontracting
  • Transportation
  • Engineering effort

If those assumptions are incomplete, the project can start with an unrealistic cost baseline.

Once execution begins, the gap gradually becomes visible.

The company may still believe it has a profitable project because the original quotation showed a healthy margin.

But the actual project may already be moving in another direction.

This is why cost control should begin at quotation—not after production starts.

Read More: What Features Should an MRP System Have for Complex Elevator Manufacturing?

7 Hidden Causes of Cost Overruns in Elevator Projects

1. Incomplete Scope During Quotation

The first source of cost leakage can be an incomplete understanding of what the project actually requires.

A quotation may account for the major elevator equipment but overlook smaller requirements that become expensive during execution.

For example:

  • Additional electrical work
  • Special mounting requirements
  • Additional structural work
  • Difficult material handling
  • Extra transportation
  • Special finishing
  • Additional site visits
  • Customer-specific components
  • Installation constraints

When these requirements emerge later, the company has two choices:

  1. Absorb the additional cost
  2. Negotiate a change with the customer

If the additional requirement is not clearly documented and commercially controlled, the project margin absorbs the difference.

This is why accurate scope definition is more than a sales activity.

It is the first layer of project cost control.

2. Engineering Changes That Reach Procurement Too Late

Engineering changes are normal in project-based elevator manufacturing.

The problem is not necessarily the change itself.

The problem is what happens after the change.

Suppose a customer changes a door configuration after the initial design.

That change could affect:

Engineering

→ revised drawings

BOM

→ changed components and quantities

Procurement

→ new purchasing requirements

Inventory

→ existing material may become surplus

Production

→ revised manufacturing requirements

Installation

→ different site requirements

Every department potentially has a cost implication.

If engineering updates the design but procurement continues using an older BOM, the company can purchase the wrong material.

If production starts using an outdated specification, rework may be required.

If installation receives incomplete information, another site visit may be necessary.

The change that looked small at the engineering stage can therefore become a much larger financial issue.

This is why engineering change management and cost control cannot be treated as separate processes.

3. BOM and Quantity Mismatches

For elevator manufacturers, the Bill of Materials is not merely a production document.

It is one of the foundations of project costing.

A BOM influences:

  • Material requirements
  • Procurement
  • Inventory
  • Production
  • Project costing
  • Installation readiness

If the BOM is inaccurate, the problem can travel through the entire project.

For example:

Incorrect BOM

↓

Incorrect MRP requirement

↓

Wrong purchasing decision

↓

Material shortage or excess

↓

Production disruption

↓

Additional procurement

↓

Project cost variance

ERPbyNet’s own material-planning approach highlights the importance of connecting BOM information with planning and material visibility rather than maintaining disconnected versions in spreadsheets.

The financial impact is important.

A missing component is not simply an inventory problem.

It can become:

Purchase cost + expedited delivery + idle labour + schedule impact + additional site expense

That is why BOM accuracy should be considered a cost-control mechanism.

4. Emergency Procurement Can Quietly Destroy Margins

Imagine that an installation team is ready to begin work.

One critical component is missing.

The planned supplier cannot deliver for another three weeks.

The project manager now has to find an alternative.

The company may end up paying:

  • A higher unit price
  • Expedited freight
  • Local sourcing premiums
  • Additional transportation
  • Supplier switching costs

And the financial impact does not stop there.

If the missing material delays installation, the company may also incur:

  • Additional manpower costs
  • Repeated travel
  • Accommodation expenses
  • Site supervision costs
  • Rescheduling costs

A procurement problem has now become a project profitability problem.

Studies of project cost and schedule performance similarly identify material shortages and procurement-related issues among important contributors to delays and overruns.

The solution is not simply “buy faster.”

The better approach is to identify potential shortages before they become emergencies.

5. Installation Delays Create More Than Schedule Problems

An installation delay is often measured in days.

But for an elevator company, those days can translate into money.

Consider a project where:

  • Materials are already purchased
  • Installation manpower has been assigned
  • Travel has been arranged
  • Site supervision is planned

Then the team discovers that the shaft is not ready.

The installation cannot proceed.

The project now requires rescheduling.

The consequences may include:

  • Idle resources
  • Additional travel
  • Additional accommodation
  • Rescheduling
  • Extended project duration
  • Delayed billing or handover=
  • Higher project cost

Recent elevator installation guidance also emphasizes site coordination and readiness as major factors in avoiding installation delays.

This demonstrates an important principle:

A project delay is often a cost event, not merely a schedule event.

6. Customer Changes Can Become Unbilled Cost

Customer requirements can change during a project.

Perhaps the customer wants:

  • A different cabin finish
  • Additional features
  • Revised doors
  • Modified dimensions
  • Additional fixtures
  • Different controls
  • Changes to the installation scope

Changes themselves are not unusual.

The danger occurs when the operational team implements them before their commercial impact is properly evaluated.

A controlled process should answer:

What changed?

Who requested it?

What material is affected?

What engineering work is required?

What additional labour is required?

What is the cost impact?

Does the customer need to approve an additional charge?

Formal project change processes commonly require changed work to be supported by detailed material, labour and other cost information before the associated adjustment is finalized.

Without such visibility, additional work can quietly become company expense.

7. Companies Often Discover the Margin Problem Too Late

This may be the most important problem of all.

Many businesses know:

Quoted Project Value

and eventually know:

Final Project Cost

But what happens between those two numbers?

That is where profitability can disappear.

Consider:

Project Cost AreaPlannedActualVariance
Material₹20 lakh₹22 lakh+₹2 lakh
Labour₹6 lakh₹7 lakh+₹1 lakh
Procurement₹2 lakh₹2.5 lakh+₹0.5 lakh
Site Expenses₹3 lakh₹4 lakh+₹1 lakh
Rework₹0.5 lakh₹1.5 lakh+₹1 lakh
Total₹31.5 lakh₹37 lakh+₹5.5 lakh

If management sees this only after project completion, there is very little corrective action available.

But if the same variance becomes visible while the project is 40% or 60% complete, management can investigate.

That changes the question from:

“Why did we lose money?”

to:

“Why is this project starting to lose margin?”

That is the difference between cost reporting and cost control.

Why Spreadsheets Struggle With Project Cost Control

Spreadsheets are useful tools.

The problem occurs when they become the primary system for managing a complex, multi-stage project.

An elevator project may involve separate spreadsheets for:

  • Quotations
  • BOQs
  • BOMs
  • Procurement
  • Inventory
  • Production
  • Installation
  • Expenses
  • Project status
  • Customer changes
  • Cost calculations

Now imagine that one specification changes.

Someone has to update multiple files.

If even one remains unchanged, the organization has multiple versions of reality.

This creates problems such as:

Delayed information

The information may be correct—but updated too late.

Duplicate data

The same project information gets entered repeatedly.

Version conflicts

Different teams may work with different BOMs or project information.

Limited traceability

It becomes difficult to determine why a cost changed.

Weak planned-vs-actual visibility

Management may see total expenses without understanding the operational reason behind them.

Manual reconciliation

Finance, procurement, stores and project teams may need to reconcile information manually.

The fundamental issue is not that spreadsheets are inherently bad.

It is that complex project operations require connected information rather than isolated records.

What Should a Modern Elevator Project Cost-Control System Track?

A strong cost-control framework should connect operational activity with financial impact.

AreaWhat Should Be Monitored?
QuotationEstimated project value and margin
ScopeIncluded and excluded requirements
EngineeringDesign revisions and changes
BOMPlanned vs revised quantities
MaterialPlanned vs actual consumption
ProcurementPlanned vs actual purchase cost
InventoryAvailability and project allocation
ProductionPlanned vs actual production requirements
LabourEstimated vs actual effort
SiteReadiness and additional site expenses
InstallationProgress, delays and resource usage
ChangesCost impact and customer approval
ReworkAdditional material and labour
ProjectPlanned vs actual total cost
ProfitabilityCurrent and projected project margin

This creates a much more complete picture.

Instead of asking only:

“How much have we spent?”

management can ask:

“Where are we spending more than planned—and why?”

How ERP Changes the Cost-Control Process

ERP becomes valuable when it connects these activities into one operational flow.

Instead of:

Quotation

→ Excel

Engineering

→ another system

BOM

→ spreadsheet

Procurement

→ separate records

Inventory

→ another database

Installation

→ manual updates

Finance

→ accounting system

the organization can create a connected project process:

Quotation → Engineering → BOM → MRP → Procurement → Inventory → Production → Installation → Actual Cost → Project Profitability

The benefit is not simply automation.

It is continuity of information.

When a change occurs upstream, the teams downstream can understand what it means for their work.

Planned Cost vs Actual Cost: The Foundation of Control

One of the most useful capabilities in project-based businesses is planned-versus-actual analysis.

Planned Cost

What the company expected the project to consume.

Actual Cost

What the project has actually consumed.

Variance

The difference between the two.

But simply showing variance is not enough.

A useful ERP environment should help management investigate the reason behind the variance.

For example:

Material Cost +12%

Why?

→ BOM changed?

→ Material price increased?

→ Excess consumption?

→ Rework?

→ Emergency procurement?

→ Material issued to wrong project?

Now the cost figure becomes actionable information.

ERP Should Connect Operational Changes to Financial Impact

This is where elevator companies can gain a significant advantage.

Suppose an engineering revision changes five components.

A connected ERP process can allow the organization to understand:

Engineering Revision

↓

BOM Revision

↓

Material Requirement Change

↓

Procurement Requirement

↓

Inventory Impact

↓

Production Impact

↓

Project Cost Impact

Without this connection, each department may see only one part of the change.

Engineering sees a drawing.

Procurement sees a purchase requirement.

Stores sees inventory.

Production sees a revised component.

Finance sees an expense.

Management sees the final variance.

ERP connects these pieces into a single project story.

From Cost Reporting to Cost Control

There is a major difference between the two.

Cost Reporting

Tells you:

“The project has exceeded its material budget.”

Cost Control

Helps you understand:

“The project is exceeding its material budget because the BOM was revised after procurement, creating additional purchases and leaving previously purchased components underutilized.”

The second statement is much more valuable.

Because now management can act.

Perhaps:

  • The change can be commercially recovered.
  • Existing inventory can be reassigned.
  • Procurement can be stopped.
  • Alternative material can be evaluated.
  • Engineering can review the design.
  • The project schedule can be adjusted.

The purpose of ERP is therefore not to guarantee that every project remains exactly within its original budget.

Complex projects will always experience changes.

The objective is to make those changes visible, traceable and actionable.

How ERPbyNet Helps Elevator Companies Improve Project Cost Control

For elevator companies, ERPbyNet is designed around the interconnected nature of project-based manufacturing and execution.

Its elevator ERP approach focuses on connecting project activities across areas such as sales, material planning, procurement, inventory, production, installation and service.

That matters because cost control cannot be isolated inside the finance department.

It begins with the operational decisions that create the cost.

From Sales to Project Execution

The project starts with customer requirements, quotation and commercial commitments.

The objective is to establish a clearer baseline before execution begins.

From BOM to Material Planning

Once engineering requirements are established, material requirements can be connected with planning and procurement.

ERPbyNet’s material-management approach emphasizes digital BOMs, demand planning and visibility into shortages and requirements.

From Procurement to Inventory

Procurement decisions can be evaluated against actual project requirements rather than being handled independently.

This helps reduce the risk of unnecessary purchases, shortages and last-minute sourcing.

From Production to Installation

Production and site activities remain part of the same project flow rather than becoming isolated operational stages.

This helps teams understand what is ready, what is pending and what could affect the project timeline.

From Project Execution to Profitability

The ultimate objective is to bring planned and actual project information together so management can understand project performance while the project is still active.

ERPbyNet specifically positions project cost and profitability visibility as a benefit for elevator companies.

What Elevator Companies Should Look for in an ERP for Cost Control

ERP features for elevator project cost control including project-based costing, multi-level BOMs, engineering revisions, material planning, procurement visibility, installation tracking, change management, and project profitability

Not every ERP is automatically suitable for elevator projects.

When evaluating an ERP, elevator companies should look beyond generic accounting and inventory features.

Ask whether the system can support:

1. Project-based costing

Can costs be tracked against individual elevator projects?

2. Multi-level BOMs

Can the system handle assemblies, subassemblies and project-specific configurations?

3. Engineering revisions

Can design changes be tracked and reflected in downstream processes?

4. Material planning

Can the system identify shortages before they become installation problems?

5. Procurement visibility

Can purchasing decisions be linked to actual project requirements?

6. Planned vs actual analysis

Can management identify cost variance during execution?

7. Site and installation tracking

Can site progress and delays be connected to project execution?

8. Change management

Can additional requirements be tracked for their operational and commercial impact?

9. Project profitability

Can management understand whether a project is still commercially healthy?

10. Cross-department visibility

Can sales, engineering, procurement, stores, production, installation and finance work from connected information?

These capabilities are more important than simply choosing an ERP with the largest feature list.

Read More: Why AI Will Fail in Elevator Companies Without the Right ERP Foundation

The Goal Is Not to Eliminate Every Cost Variance

It is unrealistic to expect complex elevator projects to operate without changes.

Customers change requirements.

Sites change.

Material prices fluctuate.

Suppliers experience delays.

Engineering requirements evolve.

Unexpected installation conditions occur.

The objective is therefore not:

Zero Variance

The objective is:

Controlled Variance

That means knowing:

  • What changed
  • When it changed
  • Why it changed
  • Which department is affected
  • What material is affected
  • What schedule impact exists
  • What additional cost may occur
  • Whether the customer needs to approve the change
  • Whether the project margin is still acceptable

That level of visibility turns project management from reactive problem-solving into proactive control.

ERPbyNet
Keep Elevator Project Costs Under Control
ERPbyNet connects project costing, BOMs, procurement, inventory, production, and installation to help elevator companies identify cost overruns earlier and protect project margins.
Elevator ERP • Project Cost Control
Improve project visibility and control costs with ERPbyNet.

Final Thoughts: The Real Problem Is Not Cost—It Is Visibility

Elevator project cost overruns rarely appear suddenly.

They usually accumulate.

A small engineering change becomes a BOM change.

The BOM change becomes a procurement requirement.

The procurement requirement creates an unexpected purchase.

The material arrives late.

Installation gets rescheduled.

The team makes another site visit.

Additional labour and travel costs are incurred.

The project takes longer.

And eventually, the company discovers that the original margin has disappeared.

The individual events may seem unrelated.

They are not.

They are connected parts of the same project lifecycle.

That is why effective cost control requires more than financial reporting at the end of a project.

It requires visibility across the processes that create the cost in the first place.

A connected ERP system can help elevator companies bring those processes together—from quotation and engineering through BOM, material planning, procurement, production, installation and project profitability.

The real advantage is not simply knowing what a project cost.

It is knowing when the project is beginning to cost more than planned—and having enough visibility to do something about it.

For elevator companies managing increasingly complex, customized and project-driven operations, that difference can determine whether growth creates more revenue—or better margins.

Explore how ERPbyNet can help connect elevator project operations and improve cost visibility.

FAQs

What causes cost overruns in elevator projects?

Common causes include inaccurate project scope, engineering changes, BOM errors, material shortages, emergency procurement, installation delays, rework, customer changes and poor visibility into actual project costs.

How can elevator companies prevent project cost overruns?

Companies can reduce the risk by establishing accurate project baselines, controlling engineering and BOM changes, planning materials early, monitoring procurement, tracking site progress and comparing planned costs with actual costs throughout execution.

How does ERP help control elevator project costs?

ERP connects quotation, engineering, BOM, material planning, procurement, inventory, production, installation and financial information, helping management identify cost variances earlier and understand their operational causes.

Why is BOM accuracy important for elevator project profitability?

The BOM influences material requirements, procurement and production. Incorrect quantities or outdated revisions can result in shortages, excess purchases, rework and additional project expenses.

Can ERP track planned vs actual project costs?

Yes. A project-focused ERP can compare estimated costs with actual material, labour, procurement, site and other project expenses, helping management identify unfavorable variances during execution.

How do engineering changes affect elevator project costs?

Engineering changes can affect BOM quantities, material requirements, procurement, production and installation. Without proper change control, the additional cost may not be identified or recovered commercially.

Can ERP help reduce installation-related cost overruns?

ERP can improve visibility into material readiness, project milestones, site activities, resources and delays, helping teams identify potential installation problems earlier.

Is ERP useful for customized elevator manufacturing?

Yes. Elevator manufacturing is highly project-driven and often involves customer-specific configurations, multi-level BOMs, engineering changes and coordinated procurement and installation. A suitable ERP can connect these processes and improve project visibility.

CategoriesERP (Enterprise Resource Planning) MRP Services for Smart Manufacturing & Production Planning | ERPbyNet

What Features Should an MRP System Have for Complex Elevator Manufacturing?

Key Takeaways

  • Complex elevator manufacturing needs more than basic MRP to manage customized products, projects, and materials.
  • Multi-level BOMs and demand explosion help calculate component and raw material requirements accurately.
  • Inventory, procurement, engineering, and production must work together for effective material planning.
  • Lead-time and project-based planning help ensure materials are available when production needs them.
  • A connected MRP system helps reduce shortages, overstocking, and reactive purchasing.

What You’ll Learn

  • Why basic MRP may not be enough for complex elevator manufacturing.
  • How multi-level BOMs and demand explosion simplify material planning.
  • How project-based planning and material allocation improve inventory decisions.
  • Why lead-time planning and shortage management are important for production.
  • How ERPbyNet’s AceMRP connects engineering, inventory, procurement, and production planning.

Real Insights

  • Physical stock does not always mean available stock because materials may already be allocated or reserved.
  • Engineering changes can change material requirements, making engineering-to-MRP integration important.
  • Knowing what material is needed is not enough; manufacturers also need to know when to procure it.
  • Exception-based planning helps teams focus on critical shortages instead of checking every material manually.
  • The right MRP system turns complex elevator orders into accurate, timely material plans.

Elevator manufacturing is rarely a simple make-and-ship process.

A single project can involve customer-specific configurations, engineering changes, multi-level BOMs, bought-out components, fabricated parts, raw materials, supplier lead times, warehouse allocation, and project-specific production requirements.

That complexity creates a fundamental challenge:

How do you make sure the right material is available, in the right quantity, at the right time—without overstocking or delaying production?

This is where a capable MRP system for elevator manufacturing becomes important.

A modern MRP system should do more than calculate material requirements. It should connect engineering, demand, BOMs, inventory, procurement, and production so manufacturers can make better material decisions before shortages become production problems.

Why Elevator Manufacturing Needs More Than Basic MRP

Traditional MRP can answer:

“What material do we need?”

But complex elevator manufacturing requires much more:

  • What is required for each elevator?
  • Which project requires it?
  • How much is already available?
  • How much is already allocated?
  • What is currently on order?
  • What needs to be manufactured internally?
  • What needs to be purchased?
  • When should procurement begin?
  • Which shortage could affect production?

For an elevator manufacturer, the planning chain often looks like:

Customer Requirement
↓
Product Configuration
↓
Engineering / BOM
↓
Material Demand
↓
MRP Calculation
↓
Procurement / Production
↓
Warehouse
↓
Project Execution

If these activities are disconnected, material planning can quickly become dependent on spreadsheets, manual calculations, and repeated communication between departments.

A suitable MRP system should bring these processes together.

Read More: Why AI Will Fail in Elevator Companies Without the Right ERP Foundation

12 Features an MRP System Should Have for Complex Elevator Manufacturing

1. Multi-Level BOM Management

An elevator is not a single-level product.

It can contain multiple assemblies, subassemblies, components, and raw materials.

For example:

Elevator
│
├── Cabin
│ ├── Cabin Frame
│ ├── Panels
│ └── Flooring
│
├── Door System
│ ├── Door Operator
│ ├── Door Panels
│ └── Sensors
│
├── Drive System
│ ├── Motor
│ ├── Controller
│ └── Related Components
│
└── Safety System
├── Safety Components
└── Associated Hardware

A capable MRP system should understand these relationships and automatically explode the BOM to calculate material requirements at different levels.

Why it matters

If an order contains 20 elevators, planners shouldn’t have to manually calculate every component required across those 20 units.

The system should be able to move from:

20 Elevators → Assemblies → Components → Raw Materials

This significantly reduces manual planning effort and the possibility of calculation errors.

2. Engineering-to-MRP Integration

Engineering-to-MRP integration connecting product configuration, BOM, MRP, procurement, and production to automatically update material requirements

Engineering changes can directly affect material requirements.

A change in:

  • Product configuration
  • Component specification
  • BOM
  • Quantity
  • Revision
  • Customer requirement

can potentially change what procurement and production need.

That’s why the MRP system should work closely with engineering data.

The ideal flow:

Engineering → BOM → MRP → Procurement → Production

Instead of engineering maintaining one version of product information while procurement works from another spreadsheet, the MRP system should use relevant approved product structures as the basis for material planning.

This creates a stronger connection between what is designed and what needs to be purchased or manufactured.

3. Demand Explosion

One of the most important capabilities of MRP is converting finished-product demand into detailed component requirements.

Suppose an elevator manufacturer receives an order for:

25 elevators

The system should determine the corresponding requirements for:

  • Subassemblies
  • Components
  • Bought-out items
  • Manufactured parts
  • Raw materials

This process is commonly referred to as BOM explosion or demand explosion.

Instead of asking the planning team to manually calculate requirements, the system performs the calculation based on the applicable product structure.

The result:

25 Elevator Orders
↓
BOM Explosion
↓
Component Requirements
↓
Net Requirements
↓
Procurement / Production Requirements

For high-volume or highly customized elevator manufacturing, this capability can become essential.

4. Project-Based Material Planning

Elevator manufacturing is often closely connected to individual customer orders and projects.

Two elevators may appear similar but have different:

  • Capacities
  • Finishes
  • Dimensions
  • Door configurations
  • Control requirements
  • Customer specifications
  • Site requirements

Therefore, material planning should not always operate only at a warehouse-wide level.

The system should help answer:

Which project needs this material?

rather than simply:

How much material is in stock?

Example

Suppose the warehouse shows:

500 units available

But:

  • 200 are allocated to Project A
  • 150 are reserved for Project B
  • 100 are required for current production

The truly available quantity may be only:

50 units

A project-aware MRP system can help planners make decisions using a more realistic view of material availability.

5. Net Requirement Calculation

A strong MRP system should not simply compare demand with physical stock.

It should consider the wider supply picture.

A typical calculation may involve:

Gross Requirement

− Available Inventory

− Relevant Incoming Supply

= Net Requirement

For example:

RequirementQuantity
Gross requirement1,000
Available inventory250
Incoming purchase orders300
Net requirement450

This helps prevent two common problems:

Over-purchasing

Buying material that is already available or incoming.

Under-purchasing

Failing to identify material that will be required later.

For complex manufacturing, accurate netting is one of the foundations of effective material planning.

6. Lead-Time-Based Planning

Knowing what is required isn’t enough.

You also need to know when to order it.

Consider a component with a supplier lead time of 45 days.

If production requires that component on:

15 November

the procurement process cannot reasonably begin in November.

The MRP system should work backward:

Required for Production
        ↓
Required Date
        ↓
Supplier Lead Time
        ↓
Planned Procurement Date

This becomes particularly important when elevator manufacturers depend on components with different supplier lead times.

A system that considers lead times can help procurement teams act earlier instead of reacting to shortages after they appear.

7. Planned Orders and Purchase Requirements

An MRP system should not stop with:

“Material shortage detected.”

That’s information.

The real value comes from turning that information into an actionable requirement.

A better process is:

This allows planners and procurement teams to move from shortage detection to planned action.

For materials that need to be manufactured internally, the system can support production requirements.

For externally sourced materials, it can support purchase requirements.

8. Material Allocation and Reservation

One of the biggest mistakes in material planning is assuming:

Physical stock = Available stock

That’s not always true.

Inventory may already be:

  • Reserved
  • Allocated
  • Committed
  • Required for another project
  • Assigned to production

For project-based elevator manufacturing, this distinction is extremely important.

Consider this:

Warehouse stock: 1,000 units

Allocated: 600 units

Available: 400 units

If an MRP system ignores allocation, it may incorrectly conclude that 1,000 units are available.

Accurate material allocation helps planners make procurement decisions based on usable supply, not just physical inventory.

9. Shortage and Exception Management

Planners shouldn’t have to manually review every material every day.

A good MRP system should help identify exceptions that need attention.

For example: <div style=”border-left:4px solid #333;padding:14px 18px;margin:20px 0;”>

<strong>Critical Material Shortage</strong><br><br>

Required: 500 units<br>
Available: 120 units<br>
Incoming: 100 units<br>
Net shortage: <strong>280 units</strong><br><br>

<strong>Action:</strong> Procurement intervention required. </div>

This kind of exception-focused planning allows teams to prioritize materials that could affect production or project schedules.

Instead of asking:

“Which of the thousands of materials should I check?”

the planner can focus on:

“Which exceptions require action today?”

10. Time-Phased Material Planning

Material requirements aren’t always needed today.

They may be required:

  • Next week
  • Next month
  • During a future production stage
  • At a specific project milestone

Therefore, an effective MRP system should consider time as well as quantity.

For example:

MaterialQuantityRequired
Component A500Week 2
Component B300Week 5
Component C150Week 8
Component D700Week 10

The total quantity isn’t enough information.

Procurement needs to know when each requirement becomes important.

Time-phased planning helps prevent:

Buying too early → Higher inventory

and

Buying too late → Production shortage

The objective is to synchronize material availability with actual requirements.

11. Make-to-Order Planning

Elevator manufacturing often involves customer-specific requirements.

This makes Make-to-Order (MTO) support an important consideration when evaluating an MRP system.

The planning chain should be capable of connecting:

Customer Order
↓
Product Configuration
↓
BOM
↓
Material Requirements
↓
Procurement / Manufacturing
↓
Production

This approach helps manufacturers plan around actual customer requirements rather than relying only on generic forecasts.

For companies handling multiple customized elevator orders, this can make material planning significantly more relevant to actual business demand.

12. Procurement, Inventory and Production Integration

Ultimately, an MRP system should not operate as an isolated planning tool.

Its real value comes from connecting the departments that act on the plan.

The connected manufacturing flow:

<div style=”text-align:center;padding:20px;margin:20px 0;border:1px solid #ddd;”>

<strong>ENGINEERING</strong><br>
↓<br>
<strong>BOM / BOQ</strong><br>
↓<br>
<strong>MRP</strong><br>
↓<br>
<strong>PROCUREMENT</strong><br>
↓<br>
<strong>WAREHOUSE</strong><br>
↓<br>
<strong>PRODUCTION</strong><br>
↓<br>
<strong>PROJECT EXECUTION</strong> </div>

When these processes are disconnected, material information can become fragmented.

When they work together, MRP can become a central planning layer connecting demand with supply.

Basic MRP vs. MRP for Complex Elevator Manufacturing

Not every system marketed as MRP software is necessarily suited to complex elevator manufacturing.

Basic MRPElevator-Focused MRP
Standard BOMMulti-level & project-specific BOM
Basic inventoryAvailable + allocated inventory
Generic demandCustomer/project-driven demand
Material calculationDemand/BOM explosion
Purchase suggestionsPlanned procurement
Basic lead timeMaterial-specific lead-time planning
Generic productionMake-to-order manufacturing
Static requirementsTime-phased requirements
Basic reportingShortage & exception management
Isolated MRPEngineering-to-procurement-to-production integration

The difference isn’t simply the number of features.

It’s whether the system can connect those features into one planning process.

Read More: How Leading Elevator Companies Deliver Better Service with the Same Workforce

How ERPbyNet’s AceMRP Fits Complex Elevator Manufacturing

ERPbyNet AceMRP for complex elevator manufacturing with BOM engineering, demand explosion, inventory planning, procurement, lead-time, manufacturing, and project-oriented planning

ERPbyNet’s AceMRP is designed around material requirements planning for manufacturing and project-driven environments.

The objective is to help manufacturers move from reactive material management toward structured planning.

Its capabilities can support areas such as:

BOM & Engineering

Use product structures and engineering requirements as the foundation for material planning.

Demand Explosion

Translate product/project requirements into detailed component-level demand.

Inventory Planning

Consider material availability while determining actual requirements.

Procurement Planning

Identify requirements and support planned purchasing before shortages disrupt execution.

Lead-Time Planning

Consider supplier lead times when determining procurement requirements.

Manufacturing Planning

Connect material requirements with manufacturing requirements.

Project-Oriented Planning

Support material planning around project and order requirements rather than treating all demand as generic inventory.

The broader objective is simple:

Know what material is required, how much is required, and when it needs to be available—before it becomes a production problem.

What Should Elevator Manufacturers Ask Before Choosing an MRP System?

Before investing in an MRP system, don’t limit your evaluation to:

“Does it have MRP?”

Ask more specific questions.

BOM & Engineering

  • Can it manage multi-level BOMs?
  • Can it handle product variants?
  • Can engineering changes flow into material planning?

Material Planning

  • Can it perform demand explosion?
  • Can it calculate net requirements?
  • Can it consider existing and incoming supply?
  • Can it support time-phased planning?

Procurement

  • Can it calculate purchase requirements?
  • Can it consider supplier lead times?
  • Can it identify upcoming shortages?

Inventory

  • Can it distinguish available, allocated and reserved stock?
  • Can material be associated with specific projects or orders?

Manufacturing

  • Can it support make-to-order requirements?
  • Can it connect material requirements with production planning?

Integration

  • Does MRP connect engineering, procurement, inventory and production?
  • Can planners work from one consistent source of material information?

These questions will reveal much more than a generic software feature checklist.

Read More: From Complaint to Closure: What Really Happens During Lift Maintenance

The Real Value of MRP in Elevator Manufacturing

The purpose of an MRP system isn’t simply to calculate numbers.

It’s to help manufacturers make better material decisions before problems reach production.

A strong system should connect:

Demand

→ Engineering

→ BOM

→ Material Requirements

→ Inventory

→ Procurement

→ Production

→ Project Execution

When that connection works properly, manufacturers can reduce reactive purchasing, improve material planning, control inventory more effectively, and identify potential shortages earlier.

ERPbyNet
Plan Complex Elevator Manufacturing with Smarter MRP
ERPbyNet helps elevator manufacturers connect BOMs, demand planning, procurement, inventory, and production to keep materials aligned with every project and manufacturing requirement.
MRP • BOM Management • Material Planning
Build a stronger material planning process with ERPbyNet.

Final Takeaway

For complex elevator manufacturing, an MRP system should be evaluated on more than basic material calculations.

The right system should understand the complexity of multi-level BOMs, customer-specific requirements, project demand, inventory allocation, supplier lead times, procurement, production and engineering changes.

The most important capabilities include:

  • Multi-level BOM management
  • Engineering-to-MRP integration
  • Demand explosion
  • Project-based planning
  • Net requirement calculation
  • Lead-time-based planning
  • Planned procurement
  • Material allocation
  • Shortage management
  • Time-phased planning
  • Make-to-order support
  • Procurement, inventory and production integration

Ultimately, the question isn’t:

“Does this software have MRP?”

The better question is:

“Can this MRP system turn a complex elevator order into an accurate, timely and actionable material plan?”

For elevator manufacturers, that’s the difference between simply managing materials and planning manufacturing intelligently.

Frequently Asked Questions About MRP for Elevator Manufacturing

What is an MRP system for elevator manufacturing?

An MRP system for elevator manufacturing helps calculate, plan, and manage the materials required to manufacture elevators based on demand, BOMs, inventory, production requirements, and procurement lead times. It helps manufacturers determine what material is needed, how much is needed, and when it is required.

Why is MRP important for elevator manufacturers?

Elevator manufacturing involves complex BOMs, customized configurations, multiple projects, bought-out components, manufactured parts, and varying supplier lead times. MRP helps connect these requirements so manufacturers can identify shortages, plan procurement, and coordinate material availability with production schedules.

What features should an MRP system have for elevator manufacturing?

Important features include multi-level BOM management, demand explosion, net requirement calculation, project-based planning, lead-time planning, planned orders, purchase requirements, material allocation, shortage management, time-phased planning, and integration with procurement and production.

Can MRP handle multi-level BOMs for elevators?

Yes. A capable MRP system should be able to manage multi-level BOMs and automatically calculate component and raw-material requirements from the finished elevator or assembly level down through lower-level components.

How does MRP help prevent material shortages?

MRP compares material demand with available inventory, allocated stock, incoming supply, and planned production or procurement. It can identify net shortages and help planners initiate procurement or manufacturing actions before the shortage affects production.

Can MRP consider supplier lead times?

Yes. Lead-time-based MRP planning helps determine when materials should be ordered based on their required production date and supplier lead time. This is particularly useful for elevator components with longer or variable procurement cycles.

Can MRP support project-based elevator manufacturing?

Yes. An MRP system designed for project-driven manufacturing can associate material requirements with specific customer orders, projects, or elevator configurations. This helps prevent material intended for one project from being incorrectly treated as universally available.

How does MRP connect engineering and procurement?

When engineering BOMs and product requirements are connected with MRP, changes in product structure can influence material requirements. The resulting requirements can then flow into procurement planning, helping purchasing teams work from current engineering and demand information.

How can ERPbyNet AceMRP help elevator manufacturers?

ERPbyNet’s AceMRP supports material requirements planning by connecting BOMs, demand, inventory, procurement, manufacturing, and project requirements. It is designed to help manufacturers move from reactive material purchasing toward structured, demand-driven planning.

CategoriesERP (Enterprise Resource Planning) Manufacturing ERP

Strategies for Managing Raw Material Demand in Complex Manufacturing

Key Takeaways

  • Complex manufacturing needs accurate material demand planning to avoid shortages and excess inventory.
  • Demand, BOMs, inventory, procurement, and production must work together for accurate planning.
  • Net material requirements are more useful than gross requirements because available and allocated stock must be considered.
  • Lead times, material criticality, and safety stock help determine when and how much to procure.
  • ERP-based planning helps manufacturers move from reactive purchasing to proactive material management.

What You’ll Learn

  • How to plan raw materials using actual demand and production requirements.
  • Why accurate multi-level BOMs are important for material planning.
  • How to calculate net material requirements using inventory and expected receipts.
  • How lead time, safety stock, and material criticality affect procurement decisions.
  • How ERPbyNet and AceMRP connect demand, inventory, procurement, and production planning.

Real Insights

  • Buying more material is not the solution; manufacturers need to know what is required and when.
  • Incorrect BOMs can cause incorrect purchasing, shortages, excess inventory, and production delays.
  • Inventory accuracy directly affects material planning and production readiness.
  • Changing customer orders can quickly change material requirements, making continuous planning important.
  • Better material planning means having the right material at the right time without tying up unnecessary working capital.

Raw material demand is rarely as simple as knowing how much material was consumed last month. In complex manufacturing, a single customer order can trigger requirements across multiple products, subassemblies, components, suppliers, warehouses, and production stages.

A change in one order can create a chain reaction:

Customer demand → Product configuration → BOM → Material requirement → Inventory availability → Procurement → Production → Delivery

When these activities are managed through spreadsheets, disconnected applications, or manual coordination, manufacturers can face two problems at the same time: material shortages that disrupt production and excess inventory that locks up working capital.

The real challenge is therefore not simply purchasing more material. It is managing raw material demand with enough visibility to know what is required, when it is required, what is already available, and what action needs to happen next.

An integrated ERP platform can help manufacturers connect sales, engineering, material planning, inventory, procurement, production, projects, and finance in one operational flow. ERPbyNet, for example, brings these functions together for manufacturing, engineering, elevator, and project-based businesses.

Why Raw Material Demand Becomes Difficult in Complex Manufacturing

Raw material demand planning challenges in complex manufacturing with multi-level BOMs, product variants, engineering changes, long-lead components, supplier dependencies, and changing production schedules

Complex manufacturing environments often deal with multi-level BOMs, product variants, make-to-order requirements, engineering changes, long-lead components, supplier dependencies, and changing customer schedules.

Consider a manufacturer receiving an order for 100 customized units.

The requirement may not stop at 100 finished products. Each product could require:

  • Multiple assemblies
  • Hundreds of components
  • Different grades of raw materials
  • Purchased parts
  • Subassemblies
  • Special long-lead components
  • Materials already allocated to other orders

If the customer later increases the order from 100 to 150 units, the material requirement changes as well.

This is why material planning should not operate as an isolated purchasing activity. It needs to be connected with demand, engineering, inventory, procurement, production, projects, and finance.

1. Start With Actual Demand, Not Just Historical Consumption

Historical consumption is useful, but it should not be the only basis for raw material planning.

A manufacturer should consider multiple sources of demand, including:

  • Confirmed sales orders
  • Open customer orders
  • Production requirements
  • Forecast demand
  • Project requirements
  • Reorder requirements
  • Existing commitments
  • Service and replacement requirements

For project-based and engineered manufacturing, this becomes even more important because demand can originate from a specific project rather than a standard production forecast.

SalesPundit can support the front end of this flow by managing leads, quotations, tender workflows, pricing, approvals, and sales activities. Once commercial requirements become actual orders, those requirements can contribute to downstream planning instead of remaining isolated in the sales department.

The objective is simple:

The material plan should reflect what the business is actually committed to producing.

2. Keep Multi-Level BOMs Accurate

A material planning system is only as reliable as the product information behind it.

If the BOM is inaccurate, the resulting material requirement can also be inaccurate.

For example:

Incorrect BOM → Incorrect material requirement → Incorrect procurement → Production disruption

Complex manufacturers may have several levels between the finished product and the raw material. A change to an assembly can therefore affect dozens or hundreds of downstream items.

A strong ERP environment should provide a controlled connection between product definitions, engineering requirements, BOMs, inventory, and material planning.

ERPbyNet’s PDS and DrawGenie capabilities can support complex product definition and engineering workflows, while AceMRP handles material planning and inventory-related requirements. This creates a stronger connection between what is being engineered and what needs to be purchased or produced.

3. Calculate Net Material Requirements

One of the biggest mistakes in material planning is treating the gross requirement as the purchase requirement.

Suppose production requires 1,000 units of a component.

That does not automatically mean procurement needs to purchase 1,000 units.

The system should consider:

Gross Requirement − Available Inventory − Allocated Stock − Expected Receipts = Net Requirement

This distinction is critical.

Without netting demand against inventory and expected receipts, manufacturers may purchase materials they already have while simultaneously overlooking materials that are genuinely short.

AceMRP is designed to connect material planning, inventory management, warehouse operations, procurement, and manufacturing coordination, helping planners work from a more connected view of requirements and availability.

4. Plan Materials According to Lead Time

A material required on the production floor on 30 September may need to be ordered weeks or months earlier.

Planning therefore needs to work backward from the requirement date.

Production requirement date
↓
Material availability date
↓
Procurement processing time
↓
Supplier lead time
↓
Purchase decision

This becomes particularly important for:

  • Imported components
  • Special-grade materials
  • Customized components
  • Single-source items
  • Long-lead electrical or mechanical parts
  • Materials with uncertain supplier availability

ERPbyNet’s MRP positioning specifically supports planning approaches for just-in-time items, long-lead materials, and materials that should be produced or procured in bulk.

The goal is not simply to identify shortages. It is to identify them early enough to do something about them.

Read More: Why Modern AMC Management Needs More Than Renewal Reminders

5. Classify Materials by Risk and Criticality

Not every raw material should be managed using the same planning rules.

A low-cost, easily available item does not carry the same business risk as a critical component with a 12-week supplier lead time.

Manufacturers can classify materials according to:

  • Criticality
  • Cost
  • Lead time
  • Supplier dependency
  • Demand variability
  • Availability
  • Substitution options
  • Production impact

For example:

Long lead time + high criticality + single supplier = high planning risk

This classification helps planners focus attention where a shortage can cause the greatest operational impact.

Instead of asking, “Which materials need replenishment?”, the better question is:

“Which material shortage could stop or delay production?”

That shift makes material planning much more strategic.

6. Use Safety Stock Intelligently

Safety stock can protect production from uncertainty, but simply increasing safety stock is not a sustainable strategy.

Too little safety stock can result in stockouts.

Too much safety stock can result in:

  • Higher carrying costs
  • Excess working capital
  • Warehouse congestion
  • Obsolescence
  • Poor inventory turnover

Safety stock decisions should therefore consider demand variability, supplier reliability, lead time, material criticality, and historical consumption.

An ERP system can make this process more practical by giving planners visibility into current stock, upcoming requirements, purchase orders, and material movements.

The objective is not maximum inventory.

The objective is appropriate inventory for the level of uncertainty and business risk.

7. Recalculate Demand When Customer Requirements Change

Complex manufacturing rarely follows a perfectly stable plan.

A customer may change:

100 units → 150 units

A project may be accelerated.

An engineering team may modify a component.

A supplier may delay a critical part.

A production schedule may move.

Each change can affect downstream material requirements.

This is where spreadsheet-based planning becomes difficult. A planner may have to manually identify which BOMs, inventory records, purchase orders, and production requirements need to be updated.

An integrated ERP environment can provide a connected view of these changes.

With ERPbyNet, SalesPundit, PDS, AceMRP, eProduction, inventory, procurement, and project-related functions can participate in a connected operational workflow.

This helps move planning from a static monthly exercise toward continuous demand management.

8. Connect Material Planning With Procurement

MRP becomes valuable only when its output leads to action.

A typical flow should look like:

Demand
↓
BOM Explosion
↓
Gross Requirement
↓
Inventory & Expected Receipts
↓
Net Requirement
↓
Planned Procurement / Production
↓
Purchase Order / Production Order
↓
Material Receipt
↓
Production

If procurement operates separately from MRP, planners may still need to communicate requirements manually.

This creates opportunities for:

  • Duplicate purchasing
  • Delayed orders
  • Incorrect quantities
  • Missed requirements
  • Poor supplier visibility
  • Emergency procurement

AceMRP brings material planning together with procurement, inventory, warehouse operations, and manufacturing coordination, supporting a more connected material flow.

9. Connect Warehouse Accuracy With Demand Planning

Even the best demand calculation becomes unreliable if the inventory data is wrong.

Imagine the ERP shows 500 components available, but only 320 are physically usable.

The planning system may conclude that there is enough material.

Production will discover otherwise.

That is why inventory accuracy is part of demand management, not a separate warehouse concern.

Barcode-enabled processes can help reduce picking and inventory errors. ERPbyNet’s AcePickerMate allows warehouse users to scan items from pick lists and supports controlled picking and unpicking through a mobile application.

The result is a stronger connection between:

System inventory → Physical inventory → Material availability → Production readiness

10. Connect Material Demand With Project and Site Requirements

For project-based manufacturers, raw material demand may be directly connected to project schedules.

An elevator manufacturer, engineering company, fabrication business, or equipment manufacturer may need materials for several projects simultaneously.

A material may be:

  • Required for Project A
  • Reserved for Project B
  • In transit for Project C
  • Available in the warehouse
  • Delayed from a supplier

Without project-level visibility, the same inventory can easily be considered available for multiple requirements.

AceSiteManager provides project execution visibility around installation schedules, activities, budgets, and site operations, while SiteApp supports project and installation activity updates from the field.

This creates an important planning advantage:

Material availability can be considered alongside project timelines rather than in isolation.

From Material Planning to Production Readiness

Raw material demand management should ultimately answer one practical question:

Will the required material be available when production needs it?

That requires coordination between planning and production.

eProduction can support production workflows, scheduling, work-center operations, labour tracking, and manufacturing visibility, while AceMRP focuses on material planning and inventory coordination.

Together, these processes help organizations identify whether a production schedule is actually supported by material availability.

Instead of discovering a shortage when production starts, planners can identify potential constraints earlier.

The Financial Impact of Better Raw Material Planning

Material planning is not only an operations issue.

It directly affects financial performance.

Excess inventory ties up cash.

Emergency purchases can increase procurement costs.

Production delays can affect delivery commitments.

Unused or obsolete materials can create write-offs.

Incorrect material consumption can distort product costing.

This is why material planning should ultimately connect with finance.

AceFinance integrates financial operations with ERPbyNet applications including AceMRP, helping inventory and manufacturing transactions flow into financial records. It supports areas such as accounts payable, accounts receivable, general ledger, fixed assets, reporting, and financial management.

This creates a more complete business picture:

Material decision → Inventory movement → Production cost → Financial impact

For management, that visibility is more valuable than a standalone inventory report.

Read More: The Hidden Relationship Between Warehousing and Customer Experience

What Manufacturers Should Look for in an ERP for Raw Material Demand Management

When evaluating manufacturing ERP software, companies should look beyond the question:

“Does the ERP have MRP?”

Instead, evaluate whether the system can connect the entire decision chain.

Look for capabilities such as:

  • Demand and order integration
  • Multi-level BOM management
  • Material requirement calculation
  • Inventory availability
  • Safety stock management
  • Lead-time planning
  • Procurement workflows
  • Production planning
  • Warehouse control
  • Barcode-based inventory processes
  • Project material visibility
  • Engineering change management
  • Cost and financial integration
  • Real-time reporting
  • Mobile operational access

The most valuable system is not necessarily the one with the longest feature list.

It is the one that connects the decisions that determine whether material will be available when and where it is needed.

How ERPbyNet Supports Connected Material Demand Management

ERPbyNet connected material demand management across sales, engineering, MRP, production, warehouse, projects, service, and finance

ERPbyNet is built around the needs of operationally complex businesses, including manufacturing, engineering, elevator, project-based, and service organizations. Its platform connects sales, projects, manufacturing, inventory, service, technicians, and finance.

For raw material demand management, different modules can contribute at different stages of the workflow:

SalesPundit helps capture and manage customer demand, quotations, pricing, and sales workflows.

PDS and DrawGenie support complex product definition and engineering requirements where product configuration can influence material requirements.

AceMRP provides the core material planning, inventory, procurement, warehouse, and manufacturing coordination layer.

eProduction connects material availability with production workflows, scheduling, work centers, and manufacturing execution.

AcePickerMate strengthens warehouse accuracy through barcode-based picking.

AceSiteManager and SiteApp help connect project execution and site requirements with operational planning.

AceService, MyAceService, and SmartTechnician become relevant when service operations generate requirements for replacement parts, maintenance materials, or field consumption. ERPbyNet provides service management, mobile service, and technician capabilities as part of its wider platform.

AceFinance connects inventory and manufacturing transactions with financial management, helping management understand the financial consequences of material decisions.

This integrated approach matters because raw material demand does not originate in the warehouse alone.

It can originate from sales, engineering, projects, production, or service.

Moving From Reactive Purchasing to Proactive Material Planning

The traditional approach to material shortages often looks like this:

Shortage discovered → Emergency purchase → Supplier follow-up → Production delay → Higher cost

A connected approach looks different:

Demand captured → BOM evaluated → Requirements calculated → Inventory checked → Shortages identified → Procurement planned → Material received → Production executed

That difference can have a direct effect on operational control.

The objective is not to eliminate every uncertainty. Manufacturing will always involve changing customer requirements, supplier variations, engineering changes, and demand fluctuations.

The objective is to make those changes visible early enough to respond intelligently.

ERPbyNet
Take Control of Raw Material Demand
ERPbyNet connects demand planning, MRP, inventory, procurement, and production to help manufacturers avoid material shortages, excess stock, and costly production delays.
MRP • Material Planning • Inventory Control
Plan materials smarter with ERPbyNet.

Final Thoughts

Managing raw material demand in complex manufacturing requires more than maintaining inventory levels.

Manufacturers need to understand what is required, why it is required, when it is required, what is already available, what is committed elsewhere, what is on order, and what could become a production constraint.

That requires a connected flow between demand, engineering, BOMs, MRP, inventory, procurement, production, projects, warehouse operations, service, and finance.

An integrated manufacturing ERP can turn these disconnected activities into one continuous planning process.

ERPbyNet is designed to bring these operational functions together for manufacturing, engineering, elevator, and project-based businesses, helping organizations improve material planning, inventory visibility, procurement coordination, production control, project execution, and financial visibility.

The goal of better raw material planning is not simply to buy the right quantity. It is to make sure the right material is available at the right time, for the right requirement, without unnecessarily tying up business capital.

When demand, inventory, procurement, production, projects, and finance work from the same connected information, manufacturers can move from reactive purchasing to proactive material planning—and from material uncertainty to greater operational control.

Frequently Asked Questions

What is raw material demand management in manufacturing?

Raw material demand management is the process of determining what materials are needed, how much is required, when they are needed, and whether available or incoming inventory can support production requirements.

Why is raw material planning difficult in complex manufacturing?

Complex manufacturing often involves multi-level BOMs, customized products, changing customer orders, long supplier lead times, multiple production stages, and project-specific requirements. These factors can make material demand change frequently.

How does ERP help manage raw material demand?

An ERP system connects demand, BOMs, inventory, MRP, procurement, production, projects, and finance. This helps manufacturers calculate material requirements, identify potential shortages, and plan procurement more effectively.

What is the role of MRP in raw material planning?

MRP calculates material requirements based on demand, BOMs, inventory, production schedules, safety stock, and lead times. It helps determine what needs to be purchased or produced and when.

How can manufacturers reduce raw material shortages?

Manufacturers can reduce shortages by maintaining accurate BOMs, monitoring inventory levels, considering supplier lead times, maintaining appropriate safety stock, and using MRP to identify upcoming material requirements before production is affected.

How can ERP help prevent excess raw material inventory?

ERP can compare upcoming demand with available inventory, allocated stock, expected receipts, and production requirements. This helps manufacturers avoid unnecessary purchases and reduce excess inventory.

Why are accurate BOMs important for material planning?

BOM accuracy directly affects material requirements. An incorrect BOM can result in wrong purchasing quantities, material shortages, excess inventory, and production delays.

Can ERP handle changes in customer demand?

Yes. An integrated ERP can help update material requirements when customer orders, quantities, product configurations, or production schedules change, allowing planners to understand their impact on procurement and production.

What should manufacturers look for in ERP software for raw material planning?

Manufacturers should consider MRP, multi-level BOM management, inventory visibility, demand planning, procurement automation, lead-time management, safety stock, production planning, warehouse management, barcode capabilities, project integration, and financial management.

How does ERPbyNet support raw material demand management?

ERPbyNet connects sales, engineering, MRP, inventory, procurement, production, warehouse, project, service, and finance processes. Its AceMRP module supports material planning and inventory management, while other ERPbyNet modules help connect demand, engineering, production, projects, warehouse operations, service, and financial activities.

CategoriesERP (Enterprise Resource Planning) ERP Solutions

Why Modern AMC Management Needs More Than Renewal Reminders

Your AMC is expiring in 30 days.

A reminder email is automatically sent to the customer.

The sales team gets a notification.

The contract appears under “Renewals Due.”

Everything looks organized.

But there is one important question:

Does anyone know whether that customer actually wants to renew?

For an elevator company, an Annual Maintenance Contract is not simply a document with a start date, end date, and renewal reminder. It represents an ongoing relationship between the service provider, the customer, and the equipment being maintained.

During that relationship, hundreds of things can happen.

Preventive maintenance visits may be completed or delayed. Breakdown calls may increase. Technicians may make repeat visits. Spare parts may be consumed. SLA commitments may be missed. Customers may raise complaints. Service quality may improve—or deteriorate.

By the time the renewal date arrives, the customer’s decision has already been influenced by all of these experiences.

That is why modern AMC management needs to go beyond renewal reminders.

A reminder tells you that a contract is ending.

Modern AMC management should tell you what happened during the contract, what is happening now, what could go wrong next, and what your team should do before the customer makes a renewal decision.

Key Takeaways

  • AMC management goes beyond renewal reminders and includes service, maintenance, customer experience, and profitability.
  • Service history and contract data help identify renewal risks before the contract expires.
  • PM visits, breakdowns, SLAs, technicians, and spare parts all affect AMC performance.
  • Connected ERP data improves AMC visibility across service, inventory, finance, and renewals.
  • Proactive AMC management improves retention, service quality, and profitability.

What You’ll Learn

  • Why renewal reminders alone are not enough for modern AMC management.
  • How service history and equipment data reveal renewal risks.
  • How to track PM visits, breakdowns, SLAs, and technician performance.
  • Why AMC profitability depends on service costs, travel, and spare-parts usage.
  • How ERPbyNet connects the complete AMC lifecycle from contract to renewal.

Real Insights

  • Two AMCs with the same renewal date can have very different renewal risks.
  • Repeated breakdowns and delayed PM visits can signal customer dissatisfaction.
  • High technician visits and spare consumption can reduce AMC profitability.
  • Connected service data helps teams act before renewal problems grow.
  • Modern AMC management is about managing the customer relationship, not just the expiry date.

What Is AMC Management Software?

AMC management software helps companies manage Annual Maintenance Contracts digitally instead of relying on spreadsheets, calendars, emails, paper records, and disconnected systems.

A typical AMC management system may help businesses manage:

  • Contract details and validity
  • Customer information
  • Equipment or asset records
  • Preventive maintenance schedules
  • Service calls
  • Breakdown complaints
  • Technician assignments
  • Service history
  • SLA commitments
  • Renewal dates
  • Billing and payment information

For elevator and lift companies, however, AMC management is more complex because a contract is closely connected with physical equipment and field service operations.

A single customer may have multiple elevators across several locations, different maintenance schedules, different service requirements, and hundreds of service interactions throughout the year.

That means the value of AMC software should not be measured only by its ability to answer:

“Which contracts are expiring?”

It should also answer:

“How healthy is each contract?”

“How well have we serviced this customer?”

“What is putting the renewal at risk?”

“How much does this AMC actually cost us to service?”

“What action should our team take next?”

That is where modern AMC management begins.

Why Renewal Reminders Alone Are Not Enough

Renewal reminders solve an important administrative problem: they reduce the possibility of forgetting a contract expiry date.

But they do not solve the operational problems that determine whether the customer will renew.

Consider a simple example.

An elevator company has an AMC with a commercial building. The contract expires next month.

The system sends the renewal reminder on time.

However, during the previous year:

  • Three preventive maintenance visits were delayed.
  • The customer raised six breakdown complaints.
  • Two complaints required repeat technician visits.
  • One critical spare part was unavailable.
  • Response time exceeded the agreed SLA twice.
  • The customer complained about poor communication.
  • The renewal proposal has not yet been discussed.

From a reminder-based system, this may simply appear as:

AMC expires in 30 days.

From a modern AMC management system, it should appear as:

AMC expires in 30 days + multiple service-risk signals require attention.

That difference is extremely important.

The first system helps you remember.

The second helps you make a decision.

The Real AMC Lifecycle Is Much Bigger Than Renewal

An AMC does not begin when the expiry reminder is generated.

It begins when the contract is created and continues through every service interaction that affects the customer’s experience.

For an elevator company, the lifecycle may look like:

Contract → Equipment → PM Planning → Technician Assignment → Service → Breakdown → Spare Parts → SLA → Customer Experience → Billing → Renewal

Every stage produces valuable information.

For example, contract information tells you what service has been promised.

Equipment information tells you which lift is being maintained.

PM information tells you whether scheduled maintenance is happening.

Breakdown information tells you how frequently the equipment is failing.

Technician information tells you how efficiently field resources are being used.

Spare-parts information tells you what materials are being consumed.

SLA information tells you whether service commitments are being met.

Customer information tells you whether the relationship is healthy.

Financial information tells you whether the contract is commercially sustainable.

If all of these activities are disconnected, the renewal team may see only the contract expiry date.

If they are connected, the company can understand the complete AMC story.

Read More: The Business Side of Lift Maintenance Nobody Talks About

5 Major Blind Spots of Reminder-Based AMC Management

Infographic showing five blind spots of reminder-based AMC management, including different customer renewal risks, missed service issues, overdue maintenance, technician travel costs, and delayed renewal proposals.

1. You Know the Expiry Date but Not the Renewal Risk

Two customers can have AMCs expiring on the same date but completely different renewal probabilities.

Customer A may have:

  • 100% PM completion
  • Fast complaint resolution
  • No major SLA issues
  • Low breakdown frequency
  • Positive service history

Customer B may have:

  • Repeated breakdowns
  • Delayed maintenance
  • Multiple complaints
  • High technician visits
  • Poor response times

A basic renewal reminder treats both customers equally.

Modern AMC management should not.

It should help the business identify which contracts are healthy and which require attention before the renewal conversation begins.

2. You Track Complaints Without Seeing the Pattern

A single breakdown does not always indicate a serious problem.

But repeated breakdowns involving the same elevator, component, or location may reveal a pattern.

For example, suppose one lift generates four complaints related to the same door system within six months.

If those complaints are treated as isolated service calls, the pattern may never become visible.

When service history is connected to equipment records, management can identify recurring problems and take preventive action.

This can improve customer experience while potentially reducing future service costs.

3. You Schedule PM Visits Without Measuring Their Completion

Preventive maintenance is one of the most important activities within an elevator AMC.

But scheduling a visit does not mean the visit actually happened.

A modern system should help answer:

  • Which PM visits are scheduled?
  • Which are completed?
  • Which are overdue?
  • Which were rescheduled?
  • Which technicians handled them?
  • What issues were identified?
  • What follow-up work is required?

Without this visibility, companies may believe they are delivering the contracted service while important maintenance activities remain incomplete.

4. You Manage Technicians Without Understanding Service Efficiency

Technician productivity directly affects AMC service costs.

Repeated travel, inefficient scheduling, repeat visits, and unnecessary delays can increase operational expenses.

For example, if a technician visits a customer three times because the required spare part was unavailable, the company is effectively paying for additional travel and technician time.

The customer may also become frustrated.

Connected AMC and field-service information helps companies identify these inefficiencies and improve scheduling, resource allocation, and service execution.

5. You Send Renewal Proposals Without Understanding the Customer Experience

A renewal proposal is a commercial document.

But renewal is fundamentally a customer decision.

Customers may ask themselves:

  • Did this company respond quickly?
  • Were maintenance visits completed on time?
  • Were breakdowns resolved properly?
  • Did technicians communicate clearly?
  • Did the elevator remain reliable?

If the answer to these questions is negative, a perfectly timed renewal email may not save the contract.

The renewal process therefore needs to start long before the expiry date.

Modern AMC Management Should Measure Contract Health

A better approach is to think about every AMC as having a measurable health status.

Instead of asking only:

“Which AMCs expire this month?”

management should ask:

“Which AMCs are healthy, which are stable, and which are at risk?”

A contract health view could consider several signals.

AMC SignalWhat It Can Reveal
PM CompletionWhether contracted maintenance is being delivered
Breakdown FrequencyWhether equipment is experiencing recurring problems
SLA ComplianceWhether service commitments are being met
Repeat ComplaintsWhether problems are being fully resolved
Technician VisitsWhether service effort is increasing
Spare ConsumptionWhether maintenance costs are rising
Customer FeedbackWhether service experience is improving
Renewal StatusWhether the commercial conversation has started
Payment StatusWhether financial issues may affect renewal
Contract ProfitabilityWhether the AMC remains commercially viable

This changes the role of AMC software.

It is no longer simply a reminder engine.

It becomes a decision-support system.

From Reactive AMC Management to Proactive AMC Management

Traditional AMC management often follows this sequence:

Expiry Approaching → Reminder → Follow-Up → Proposal → Renewal

The problem is that most action happens near the end of the contract.

A proactive model starts much earlier:

Monitor → Identify Risk → Take Action → Improve Service → Engage Customer → Renew

Imagine an AMC that expires in 60 days.

Instead of waiting until the final month, the system identifies:

  • Two overdue PM visits
  • Three recent breakdowns
  • One unresolved complaint
  • High spare consumption
  • Poor SLA performance

That information creates an opportunity.

The company can resolve the service issues before discussing renewal.

The conversation changes from:

“Your AMC is expiring. Would you like to renew?”

to:

“We noticed recurring issues with this elevator and have already scheduled corrective action to improve reliability.”

That is a completely different customer experience.

Why This Matters Even More for Elevator Companies

Elevator maintenance is highly dependent on field operations.

Unlike a simple subscription contract, an elevator AMC is connected to physical assets that require continuous attention.

A single AMC may involve:

  • Multiple lifts
  • Different equipment models
  • Multiple customer locations
  • Preventive maintenance schedules
  • Emergency breakdowns
  • Technician assignments
  • Travel
  • Spare parts
  • Service reports
  • SLA commitments
  • Customer communication
  • Recurring billing
  • Renewal proposals

This creates a significant amount of operational data.

The challenge is not necessarily a lack of data.

The challenge is connecting the data.

The sales team may know that the AMC is expiring.

The service team may know that complaints are pending.

The technician may know that the same elevator has recurring issues.

The warehouse team may know that a specific spare part is frequently unavailable.

Finance may know that invoices are overdue.

Management needs to see all of these signals together.

That is why AMC management should not operate as an isolated department.

AMC Management Is Also a Profitability Problem

Renewing an AMC is good.

Renewing a profitable AMC is better.

Consider two contracts with the same annual value.

MetricContract AContract B
Annual AMC Value₹2,00,000₹2,00,000
Breakdown CallsLowHigh
Technician VisitsLowHigh
Travel CostLowHigh
Spare ConsumptionNormalHigh
SLA IssuesFewFrequent
Service EffortControlledIntensive
ProfitabilityHealthyAt Risk

From a sales perspective, both contracts are worth ₹2,00,000.

From an operational perspective, they are very different businesses.

This is why modern AMC management should connect contract information with service and financial data.

Companies can then identify:

  • High-value customers
  • High-cost contracts
  • Frequently serviced equipment
  • Contracts with excessive spare consumption
  • Contracts affected by SLA penalties
  • Contracts that may require repricing
  • Contracts that could benefit from modernization
  • Contracts with strong renewal potential

This moves AMC management from administrative tracking to business intelligence.

How ERPbyNet Helps Modernize AMC Management

Infographic showing how ERPbyNet connects sales, AMC contracts, service teams, technicians, inventory, customer information, billing, and finance for elevator companies.

ERPbyNet takes a broader approach to managing project-based and engineering business operations, including the requirements of elevator companies.

Instead of treating the AMC as a standalone record, ERPbyNet can connect the activities that surround the contract and customer relationship.

This can include:

  • Contract and AMC management
  • Preventive maintenance planning
  • Service calls and complaints
  • Technician operations
  • Service history
  • Spare-parts visibility
  • Customer information
  • Billing processes
  • Financial information
  • Renewal workflows

The advantage of this connected approach is simple.

The renewal team does not have to work with one set of information while the service team works with another.

The same customer and equipment information can support multiple business functions.

For example:

  • Sales can understand renewal status and customer history.
  • Service teams can monitor PM schedules, complaints, and breakdowns.
  • Technicians can receive assigned work and update service information from the field.
  • Inventory teams can understand spare usage and material requirements.
  • Finance teams can connect contract activity with billing and financial processes.
  • Management can gain a broader view of service performance, operational costs, and contract profitability.

The objective is not simply to send renewal reminders faster.

The objective is to create a stronger operational foundation for customer retention.

Read More: How Leading Elevator Companies Deliver Better Service with the Same Workforce

What Should You Look for in AMC Management Software?

If you are evaluating AMC management software, don’t make automatic reminders your main selection criterion.

Ask these questions instead.

Contract Management

Can the system:

  • Track every active AMC?
  • Store contract terms and coverage?
  • Link contracts to specific elevators or equipment?
  • Track expiry, renewal, and cancellation?
  • Maintain historical contract information?

Preventive Maintenance

Can it:

  • Automatically plan PM activities?
  • Track scheduled and completed visits?
  • Highlight overdue maintenance?
  • Maintain service history?
  • Monitor maintenance performance across locations?

Breakdown and Service Management

Can it:

  • Record customer complaints?
  • Link complaints to equipment?
  • Track response and resolution time?
  • Identify repeat breakdowns?
  • Monitor SLA performance?

Technician Management

Can it:

  • Assign work based on availability?
  • Provide technicians with relevant service information?
  • Capture field updates?
  • Track service activity?
  • Reduce unnecessary repeat visits?

Spare-Parts Management

Can it:

  • Track parts consumed during service?
  • Connect material usage to equipment?
  • Identify frequently used parts?
  • Improve material availability?
  • Help reduce service delays caused by stock shortages?

Renewal Management

Can it:

  • Identify upcoming renewals?
  • Create renewal workflows?
  • Track proposal status?
  • Show customer service history before renewal?
  • Highlight contracts that require attention?

Financial Visibility

Can it:

  • Connect AMC billing with finance?
  • Track receivables?
  • Monitor contract revenue?
  • Understand service-related costs?
  • Help identify profitable and loss-making contracts?

If your answer to these questions is yes, you are moving beyond basic AMC tracking.

You are moving toward complete AMC lifecycle management.

The Future of AMC Management Is Proactive

The future of AMC management is not about sending more emails.

It is about making better decisions earlier.

Instead of knowing only:

“This AMC expires next month.”

a modern system should help you understand:

“This AMC expires next month, all preventive maintenance visits are complete, breakdown frequency is low, there are no unresolved complaints, the renewal proposal has been sent, and the customer relationship is healthy.”

It should also identify the opposite scenario:

“This AMC expires next month, two PM visits are overdue, breakdown frequency has increased, a complaint remains unresolved, and service costs are rising.”

The second scenario requires action.

Without connected information, management may discover the problem only after the customer decides not to renew.

With better visibility, the company has time to intervene.

That is the real value of modern AMC management.

Final Takeaway: Don’t Just Manage the Expiry Date

Renewal reminders are useful.

But they are only one small part of the AMC lifecycle.

For elevator companies, effective AMC management should connect:

Contract → Equipment → Maintenance → Service → Technician → Spare Parts → Customer → Finance → Renewal

When these activities work together, companies can move beyond reactive contract administration.

They can improve preventive maintenance.

They can identify recurring service problems.

They can improve technician utilization.

They can control service costs.

They can understand customer experience.

And most importantly, they can approach renewal conversations with much better information.

Because the real question is not:

“Did we remind the customer that their AMC is expiring?”

The better question is:

“Did we manage the customer relationship well enough to make renewal the obvious choice?”

That is the difference between managing an AMC and managing the relationship behind it.

And for modern elevator companies, that difference can have a direct impact on service quality, customer retention, operational efficiency, and profitability.

ERPbyNet
Go Beyond AMC Renewal Reminders
ERPbyNet helps elevator companies manage AMC renewals, service schedules, contracts, technicians, customer follow-ups, and service performance from one connected platform.
AMC Management • Service Operations
Manage the complete AMC lifecycle with ERPbyNet.

Frequently Asked Questions About AMC Management Software

1. What is AMC management software?

AMC management software helps businesses manage Annual Maintenance Contracts from one platform. It can track contracts, customers, equipment, preventive maintenance, service requests, technicians, complaints, renewals, and billing, giving service teams better visibility throughout the contract lifecycle.

2. Why is AMC management software important for elevator companies?

Elevator companies manage recurring maintenance, breakdown calls, technicians, spare parts, SLAs, and customer relationships. AMC software connects these activities, helping companies reduce missed maintenance, improve service response, track equipment history, and manage renewals more effectively.

3. Is AMC software only used for renewal reminders?

No. Renewal reminders are only one part of AMC management. Modern AMC software can also manage preventive maintenance, breakdowns, service calls, technician assignments, equipment history, SLA tracking, spare parts, customer information, and renewal workflows.

4. How does AMC software help improve customer retention?

AMC software provides visibility into service quality before the renewal date. Companies can identify delayed maintenance, repeated breakdowns, unresolved complaints, or SLA issues early and take corrective action before these problems affect the customer’s renewal decision.

5. Can AMC software manage preventive maintenance?

Yes. AMC software can help schedule and track preventive maintenance visits, assign technicians, monitor completed and overdue activities, and maintain service history. This helps elevator companies ensure that contracted maintenance activities are performed on time.

6. Can AMC management software help control service costs?

Yes. By connecting service activity with technician visits, travel, breakdowns, and spare-parts consumption, AMC software can help companies identify contracts that require excessive resources and understand where service costs can be reduced.

7. What should I look for in AMC management software?

Look for features that cover the complete AMC lifecycle, including contract management, preventive maintenance, service and breakdown management, technician scheduling, equipment history, SLA tracking, renewal management, inventory visibility, and financial integration.

8. What is the difference between AMC software and ERP?

AMC software primarily focuses on managing maintenance contracts and related service activities. An ERP connects AMC operations with wider business functions such as sales, projects, inventory, procurement, technicians, and finance, providing a more integrated view of the business.

9. Can ERPbyNet manage the complete AMC lifecycle?

ERPbyNet is designed to connect AMC and service operations with other business processes. For elevator companies, this can provide a connected view across contracts, preventive maintenance, service calls, technicians, spare parts, customer information, billing, and renewal activities.

CategoriesAI-Powered ERP ERP (Enterprise Resource Planning)

Why AI Will Fail in Elevator Companies Without the Right ERP Foundation

Key Takeaways

  • AI cannot succeed without a strong ERP foundation.
  • Disconnected data and manual processes produce inaccurate AI insights.
  • Clean ERP data enables reliable AI predictions for maintenance, inventory, and operations.
  • Integrated ERP provides the visibility AI requires to support better business decisions.
  • Elevator companies should strengthen ERP before adopting AI to achieve long-term success.

What You’ll Learn

  • Why ERP is the foundation for successful AI adoption.
  • How poor ERP data affects AI accuracy.
  • The role of real-time ERP data in predictive maintenance and planning.
  • Common mistakes elevator companies make when implementing AI.
  • How ERPbyNet prepares elevator businesses for AI with connected operations and clean data.

Real Insights

  • AI exposes operational weaknesses instead of fixing them automatically. :contentReference[oaicite:0]{index=0}
  • Incomplete service records and inaccurate inventory reduce AI reliability. :contentReference[oaicite:1]{index=1}
  • Standardized ERP processes improve AI performance across departments. :contentReference[oaicite:2]{index=2}
  • Real-time ERP visibility enables smarter AI-driven decisions for maintenance, scheduling, and resource planning. :contentReference[oaicite:3]{index=3}
  • Successful AI starts with trusted ERP data, not advanced algorithms. :contentReference[oaicite:4]{index=4}

Artificial Intelligence (AI) is quickly becoming one of the biggest topics in the elevator industry. From predictive maintenance and intelligent scheduling to automated customer support and service optimization, AI promises to transform how elevator companies operate.

Many business owners believe that adopting AI is simply a matter of purchasing the latest software or integrating a chatbot into their operations. In reality, AI is not a magic solution that automatically fixes inefficient processes, disconnected systems, or poor-quality data.

For elevator companies, AI is only as effective as the business information it learns from. If technician records are incomplete, spare parts inventories are inaccurate, customer histories are scattered across spreadsheets, and service operations rely on manual processes, AI will only make poor decisions faster.

This is why many AI initiatives fail—not because the technology isn’t powerful, but because the business lacks the operational foundation needed to support it.

That foundation is an integrated Enterprise Resource Planning (ERP) system.

An ERP connects every critical business function—from sales and project execution to installation, maintenance, inventory, finance, and customer service—into one centralized platform. Instead of isolated data and disconnected workflows, every department works from a single source of truth.

In this article, we’ll explore why AI alone cannot transform elevator companies, why ERP is the missing foundation behind successful AI adoption, and how businesses can prepare today for the next generation of intelligent operations.

AI Is Transforming the Elevator Industry—But Not in the Way Most Companies Think

The elevator industry has always been driven by operational efficiency. Every day, companies manage installation projects, preventive maintenance schedules, Annual Maintenance Contracts (AMCs), emergency breakdowns, technician dispatching, spare parts inventory, compliance inspections, and customer communications—all while trying to deliver fast, reliable service.

As AI technologies become more accessible, many companies are exploring how they can improve these operations.

Potential applications include:

  • Predicting equipment failures before they occur
  • Optimizing technician schedules based on skills and location
  • Forecasting spare parts demand
  • Automating service prioritization
  • Generating maintenance insights from historical service records
  • Assisting customer support through AI-powered chatbots
  • Improving decision-making with predictive analytics

These possibilities are exciting, and many software vendors market AI as a shortcut to operational excellence.

However, this creates a dangerous misconception.

AI does not replace operational discipline.

It doesn’t automatically organize years of inconsistent service records.

It cannot understand incomplete maintenance histories.

It won’t correct inaccurate inventory counts.

It cannot identify missing customer information that has never been recorded.

Instead, AI depends entirely on the quality, consistency, and completeness of the information it receives.

Think of AI as a highly intelligent analyst. Give it complete, reliable, and structured business data, and it can uncover valuable insights. Feed it inconsistent spreadsheets, duplicated customer records, or disconnected systems, and its recommendations become unreliable.

For elevator companies, this distinction is critical.

The future belongs not to businesses that simply “adopt AI,” but to those that first build an operational environment where AI can succeed.

The Biggest AI Mistake Elevator Companies Are Making

Nine-slide infographic explaining why AI projects fail in elevator companies without connected ERP systems, clean data, standardized processes, and integrated business operations.

Many elevator businesses are rushing toward AI because they fear being left behind.

Unfortunately, they often begin with the wrong question.

Instead of asking:

“How can we prepare our business for AI?”

They ask:

“Which AI tool should we buy?”

The difference may seem small, but it completely changes the outcome.

Technology alone cannot solve operational problems that already exist inside the business.

Imagine an elevator company where:

  • Service requests arrive through phone calls, WhatsApp, emails, and handwritten notes.
  • Technician schedules are maintained manually.
  • Customer equipment history exists in multiple Excel files.
  • Spare parts inventory isn’t updated in real time.
  • AMC renewals depend on manual reminders.
  • Installation projects are tracked independently from service operations.

Now imagine introducing AI into this environment.

Can AI predict failures accurately?

Can it recommend the right technician?

Can it estimate spare parts demand?

Can it calculate maintenance trends?

The answer is simple: not consistently.

AI learns from patterns. If the underlying data is incomplete or inconsistent, the patterns it identifies are equally flawed.

This is one of the biggest reasons AI projects fail across industries.

Businesses invest in sophisticated technology while ignoring the operational systems that generate the data AI depends on.

For elevator companies, the biggest mistake isn’t delaying AI adoption.

The biggest mistake is trying to implement AI before establishing a connected digital foundation.

Why AI Cannot Fix Broken Business Processes

Artificial intelligence excels at analyzing information and identifying patterns.

What it cannot do is repair inefficient workflows that generate poor information in the first place.

Consider a typical elevator service operation.

A customer reports an issue.

The coordinator manually assigns a technician.

The technician visits the site and records observations on paper.

Later, those notes are manually entered into another system.

Inventory updates happen separately.

Invoices are generated elsewhere.

Customer history is stored in different locations.

Every manual handoff increases the likelihood of delays, missing information, duplicate records, and human error.

Now imagine asking AI to optimize this workflow.

It faces several challenges:

AI Cannot Create Data That Doesn’t Exist

If previous maintenance visits were never recorded digitally, AI has no historical knowledge to analyze.

Without historical service records, predicting future failures becomes impossible.

AI Cannot Trust Inaccurate Information

Suppose your inventory system indicates ten brake components are available.

In reality, only four remain because inventory wasn’t updated after previous service visits.

AI will confidently recommend maintenance schedules based on incorrect stock levels.

The recommendation sounds intelligent—but it’s based on false information.

AI Cannot Connect Disconnected Departments

Sales teams, installation teams, finance departments, warehouse staff, and field technicians often use separate tools.

Without integration, AI sees fragmented pieces instead of the complete customer journey.

It may optimize one department while unintentionally creating problems in another.

For example:

  • Sales promises faster installation.
  • Procurement doesn’t receive updated material requirements.
  • Projects are delayed.
  • Service schedules change.
  • Customer satisfaction declines.

AI didn’t cause the problem.

Disconnected operations did.

AI Cannot Replace Standardized Processes

One technician records detailed service reports.

Another writes only a few words.

A third technician skips documentation entirely.

When service quality varies significantly between employees, AI cannot reliably identify equipment trends.

Consistency is essential before intelligence becomes valuable.

Standardized digital workflows create reliable information.

Reliable information enables better AI decisions.

Read More: How Leading Elevator Companies Deliver Better Service with the Same Workforce

Why ERP Is the Foundation AI Depends On

Artificial Intelligence is often compared to the brain of a modern business.

If that’s true, ERP is the nervous system.

Without a connected nervous system, even the most intelligent brain cannot function effectively.

An ERP platform brings together every operational activity into one integrated environment.

Instead of maintaining separate systems for sales, projects, service management, inventory, procurement, finance, and customer support, information flows automatically across departments.

This creates something AI values above everything else:

Trusted business data.

When an elevator company operates through a centralized ERP system, every activity contributes to a continuously growing knowledge base.

For example:

Every Service Visit Becomes Useful Intelligence

Each technician visit captures valuable operational data, including:

  • Equipment history
  • Failure types
  • Parts replaced
  • Repair duration
  • Technician observations
  • Customer signatures
  • Service completion times

Over time, these records create rich historical data that AI can analyze to identify recurring faults, predict equipment failures, and improve maintenance planning.

Inventory Reflects Operational Reality

ERP automatically updates spare parts inventory as materials move through procurement, warehouses, installation projects, and service activities.

Instead of relying on assumptions, AI can recommend maintenance plans based on actual stock availability, helping businesses reduce emergency shortages and unnecessary overstocking.

Customer Information Remains Connected

Every quotation, project milestone, installation record, AMC agreement, maintenance visit, complaint, invoice, and payment becomes part of a single customer profile.

This gives AI complete business context rather than isolated transactions.

Instead of answering simple questions, AI begins supporting better business decisions.

Departments Start Speaking the Same Language

One of the biggest challenges in elevator companies is information fragmentation.

Sales focuses on new projects.

Project managers monitor installations.

Service teams manage maintenance.

Warehouse staff control inventory.

Finance tracks invoices and payments.

Without ERP, each department builds its own version of reality.

ERP eliminates these silos by creating one shared operational platform.

Once everyone works from the same information, AI can analyze the entire business instead of isolated departments.

That is where meaningful intelligence begins.

Real-World Scenarios Where AI Fails Without ERP

The conversation around AI often focuses on what the technology can do. However, business leaders should pay equal attention to understanding where AI fails. In the elevator industry, AI doesn’t fail because of poor algorithms—it fails because it lacks access to complete, reliable, and connected operational data.

Let’s examine some real-world scenarios.

AI Recommends the Wrong Technician

An AI-powered scheduling system is designed to assign the most suitable technician based on expertise, location, and availability.

On paper, this sounds straightforward.

However, imagine these common situations:

  • Technician skills haven’t been updated for months.
  • Leave records exist in HR software but aren’t connected to service scheduling.
  • Current job assignments are tracked manually.
  • Travel time isn’t considered.
  • Technician certifications are stored separately.

The AI assigns the “best” technician according to outdated information.

The result?

  • Delayed service response
  • Increased travel costs
  • Missed service-level agreements (SLAs)
  • Frustrated customers
  • Reduced technician productivity

An integrated ERP continuously updates technician availability, skills, certifications, work orders, GPS location, and job completion status, giving AI accurate information to make better scheduling decisions.

Predictive Maintenance Produces False Alerts

Predictive maintenance is one of AI’s most promising applications.

The goal is simple: identify equipment that is likely to fail before it actually does.

But prediction requires history.

Consider an elevator installed eight years ago.

Over those years:

  • Some service visits were recorded digitally.
  • Others exist only in paper files.
  • Several maintenance reports were lost.
  • Spare part replacements weren’t documented consistently.
  • Emergency breakdowns weren’t categorized properly.

When AI analyzes this incomplete history, it cannot accurately identify failure patterns.

Instead of preventing breakdowns, it generates unreliable recommendations.

A connected ERP ensures every inspection, repair, replacement, technician note, customer complaint, and maintenance activity becomes part of the equipment’s digital history, significantly improving predictive accuracy over time.

Inventory Forecasting Goes Wrong

AI can forecast spare parts demand by analyzing consumption patterns.

However, forecasting only works when inventory data reflects reality.

Suppose the warehouse system shows:

  • 25 door sensors available
  • 18 brake assemblies in stock
  • 40 control relays ready for dispatch

In reality:

  • Some parts have already been used.
  • Others were reserved for ongoing projects.
  • A few were damaged but never removed from inventory.
  • Several purchase orders remain pending.

AI now believes inventory is sufficient.

Emergency service requests arrive.

Technicians reach customer sites without required components.

Projects are delayed.

Customers wait longer.

The issue wasn’t AI.

The issue was inaccurate operational data.

ERP continuously synchronizes procurement, warehouse operations, project consumption, service usage, and inventory movements, giving AI trustworthy information for forecasting.

Customer Support Becomes Less Intelligent

Many businesses introduce AI chatbots hoping to improve customer experience.

But what happens when a customer asks:

“Has my lift been serviced this month?”

If customer history exists across multiple systems, the chatbot cannot answer accurately.

Similarly:

  • It cannot verify warranty status.
  • It cannot check AMC validity.
  • It cannot identify open service requests.
  • It cannot estimate technician arrival time.

Customers quickly lose confidence.

When ERP centralizes customer information, AI can provide faster, more accurate, and context-aware responses.

Five Signs Your Elevator Company Isn’t AI-Ready

Infographic highlighting five signs an elevator company is not AI-ready, including Excel dependency, disconnected departments, paper reports, siloed customer data, and decisions made without real-time data.

Many organizations believe they are ready for AI simply because they have digital tools.

Digital tools alone do not create AI readiness.

Ask yourself these questions.

1. Is Your Business Still Dependent on Excel?

If operational decisions depend on spreadsheets rather than integrated systems, AI will struggle to produce reliable insights.

2. Does Customer Information Exist in Multiple Places?

When sales, service, finance, and projects maintain separate customer records, AI cannot build a complete customer profile.

3. Are Technicians Still Completing Paper Reports?

Paper documentation delays data availability and reduces AI’s ability to learn from field operations.

4. Do Departments Operate Independently?

Disconnected teams create disconnected data.

AI performs best when every department contributes to one unified information system.

5. Are Business Decisions Based on Assumptions Instead of Real-Time Data?

If managers frequently ask:

  • Which AMCs expire this month?
  • Which technicians are available?
  • Which spare parts are running low?
  • Which projects are delayed?

…and the answers require phone calls, emails, or manual reports, AI will inherit the same operational uncertainty.

Building an AI-Ready Elevator Business Starts with ERP

Rather than asking,

“Which AI solution should we implement?”

A better question is:

“Is our business generating the kind of data AI can trust?”

The answer depends on how information flows through your organization.

A modern ERP creates a continuous digital thread connecting every stage of elevator operations.

Sales and Quotation

Every inquiry, quotation, and customer interaction becomes structured data instead of isolated documents.

Project Execution

Engineering, procurement, installation, budgeting, and project milestones remain connected from start to finish.

Field Service

Technicians receive digital work orders, update job status in real time, capture service reports, record parts usage, and complete customer acknowledgments from the field.

AMC Management

Renewals, preventive maintenance schedules, compliance activities, billing, and customer communication remain synchronized automatically.

Inventory and Procurement

Warehouse stock, purchase planning, vendor management, and spare parts consumption remain continuously updated.

Finance

Invoices, payments, contracts, expenses, and profitability remain connected with operational activities.

Together, these connected workflows produce something far more valuable than automation.

They produce high-quality operational intelligence.

And that is exactly what AI requires.

How ERPbyNet Creates the Right Foundation for AI

Successful AI adoption doesn’t begin with artificial intelligence.

It begins with operational excellence.

ERPbyNet is designed specifically for project-based and elevator businesses where installations, service operations, AMC management, inventory, finance, and field teams must work together seamlessly.

Instead of isolated applications, ERPbyNet creates one connected platform where business information flows automatically across departments.

This foundation supports future AI initiatives by ensuring that every operational event contributes to a centralized knowledge base.

With ERPbyNet, elevator companies can:

  • Digitize service operations and technician reporting
  • Centralize customer and equipment history
  • Manage preventive maintenance and AMC workflows
  • Track spare parts in real time
  • Improve project visibility
  • Connect finance with operations
  • Standardize business processes
  • Generate reliable operational data for future AI applications

Rather than treating AI as a separate investment, ERPbyNet helps businesses prepare the operational environment where AI can deliver measurable business value.

Read More: The Hidden Relationship Between Warehousing and Customer Experience

The Next Five Years Will Separate AI Users from AI-Ready Businesses

Over the next decade, AI will become a standard capability across the elevator industry.

Predictive maintenance, intelligent scheduling, automated reporting, demand forecasting, and decision support will become increasingly common.

The companies that succeed, however, won’t necessarily be those that buy AI first.

They will be the ones that prepare their business first.

Organizations with connected operations, standardized workflows, reliable business data, and integrated ERP systems will adopt AI faster, achieve better results, and avoid costly implementation failures.

Those relying on spreadsheets, disconnected applications, and manual processes may invest heavily in AI but struggle to generate meaningful outcomes.

The competitive advantage will not come from owning AI.

It will come from owning high-quality operational data.

Conclusion

AI has the potential to transform the elevator industry—but only when it’s built on the right foundation. Without connected data, standardized processes, and real-time operational visibility, AI becomes an expensive tool with limited business impact.

Before investing in AI, invest in the system that powers it.

ERPbyNet helps elevator companies unify project management, installation, AMC management, field service, inventory, procurement, finance, and customer data into a single ERP platform—creating the reliable foundation AI needs to deliver accurate insights and smarter decisions.

Don’t let disconnected systems hold back your AI journey. Build a future-ready business with an ERP designed specifically for the elevator industry.

Ready to make AI work for your business instead of against it?

Schedule a personalized demo and discover how ERPbyNet can help you streamline operations, improve service performance, and prepare your business for the next generation of AI-driven innovation.

👉 Visit https://erpbynet.com/ today and take the first step toward an AI-ready elevator business.

ERPbyNet
Build the ERP Foundation Your AI Strategy Needs
ERPbyNet unifies service, projects, inventory, finance, and customer data—creating the reliable foundation AI needs to deliver accurate insights and smarter automation.
AI-Ready ERP • Unified Business Data
Start your AI journey with ERPbyNet.

Frequently Asked Questions

Can AI replace ERP software?

No. AI and ERP serve different purposes. ERP manages and centralizes business operations, while AI analyzes operational data to generate insights, predictions, and recommendations. AI performs best when supported by a well-implemented ERP system.

Why does AI need ERP data?

AI depends on structured, accurate, and connected data to identify patterns and make intelligent decisions. ERP provides that centralized business information across departments.

Is AI useful for elevator maintenance companies?

Yes. AI can improve predictive maintenance, technician scheduling, inventory forecasting, customer service, and operational analytics. However, these benefits depend on having reliable operational data available.

What should elevator companies do before investing in AI?

Before implementing AI, companies should digitize their operations, standardize workflows, centralize customer and equipment data, and implement an integrated ERP platform that connects every department.

CategoriesElevator Maintenance Management ERP (Enterprise Resource Planning)

How Leading Elevator Companies Deliver Better Service with the Same Workforce

Key Takeaways

  • Leading elevator companies increase service capacity without hiring more technicians by optimizing scheduling, workflows, and field operations.
  • Real-time technician visibility reduces travel time and idle hours, allowing more service calls to be completed each day.
  • Digital access to service history and spare parts information improves first-time fix rates and minimizes repeat visits.
  • Integrated ERP connects service, AMC, inventory, finance, and customer management into one centralized platform.
  • Smarter operations improve customer satisfaction, technician productivity, and long-term business growth without expanding the workforce.

What You’ll Learn

  • How successful elevator companies handle more service requests with the same workforce.
  • Why smart scheduling, technician coordination, and preventive maintenance increase operational efficiency.
  • How ERP eliminates manual processes and disconnected systems that slow service delivery.
  • The importance of real-time visibility into technicians, inventory, and service performance.
  • How ERPbyNet helps elevator businesses improve productivity without increasing headcount.

Real Insights

  • The most productive elevator companies don’t necessarily employ more technicians—they manage them more efficiently.
  • Many lost service hours result from poor scheduling, incomplete job information, and unavailable spare parts, not technician performance.
  • Centralized ERP enables managers to monitor workloads, response times, and field activities in real time.
  • Connected departments reduce communication gaps, helping service, inventory, and finance teams work together seamlessly.
  • Businesses that digitize service operations are better positioned to scale while maintaining consistent service quality.

The elevator industry is facing a challenge that almost every service-focused business recognizes: customer expectations continue to rise while skilled technicians remain difficult to find.

Building owners expect faster response times. Facility managers demand proactive maintenance. Service Level Agreements (SLAs) are becoming stricter, and unplanned breakdowns can quickly damage customer trust.

For many elevator companies, the first instinct is to hire more technicians. While expanding the workforce may seem like the obvious solution, it is often the most expensive—and not always the most effective—approach.

Interestingly, many of the industry’s top-performing companies are achieving something different. Instead of continuously increasing headcount, they are delivering more maintenance visits, resolving service calls faster, reducing repeat breakdowns, and improving customer satisfaction with nearly the same workforce.

So, what are they doing differently?

The answer lies in operational efficiency rather than workforce expansion.

This article explores the practical strategies leading elevator companies use to improve service productivity, reduce operational bottlenecks, and create a scalable service organization. You’ll also discover why integrated business systems have become one of the biggest competitive advantages in the modern elevator industry.

The Real Challenge Isn’t a Lack of Technicians

Across the elevator industry, companies commonly face challenges such as:

  • Increasing numbers of installed elevators under maintenance
  • Rising customer expectations for faster service
  • Difficulty recruiting experienced field technicians
  • Higher travel costs
  • Delays caused by unavailable spare parts
  • Growing administrative workload
  • Multiple disconnected software systems
  • Increasing compliance requirements

Many organizations interpret these issues as a staffing problem.

In reality, they’re often productivity problems.

A technician spending two hours driving across the city due to poor scheduling isn’t creating value.

A service engineer waiting for unavailable spare parts isn’t repairing elevators.

A supervisor manually assigning jobs through phone calls and spreadsheets isn’t optimizing workforce utilization.

In many businesses, technicians spend a significant portion of their working day on activities that don’t involve actual maintenance or repairs.

Reducing this operational waste can dramatically increase service capacity without hiring additional employees.

Why Hiring More Technicians Isn’t Always the Best Solution

Comparison infographic showing how two elevator service companies with the same 25 technicians achieve different results through intelligent scheduling, mobile field applications, real-time spare parts visibility, and connected service operations.

Recruiting experienced elevator technicians has become increasingly difficult.

Beyond recruitment costs, companies must also invest in:

  • Training
  • Certifications
  • Safety compliance
  • Equipment
  • Vehicles
  • Travel expenses
  • Payroll
  • Ongoing skill development

Even after making these investments, inefficient internal processes can continue limiting productivity.

Consider this example.

Company A

  • 25 technicians
  • Manual scheduling
  • Paper-based service reports
  • Inventory managed separately
  • Procurement disconnected from service
  • Customer history stored across multiple systems

Result:

  • Longer response times
  • Frequent repeat visits
  • High overtime costs
  • Lower technician utilization

Company B

  • 25 technicians
  • Intelligent scheduling
  • Mobile field applications
  • Real-time spare parts visibility
  • Automated maintenance planning
  • Connected service operations

Result:

  • More jobs completed each day
  • Faster first-time fixes
  • Lower operating costs
  • Higher customer satisfaction

Both companies employ the same number of technicians.

The difference lies in how effectively they use them.

What Leading Elevator Companies Do Differently

Successful elevator service organizations don’t rely on harder work—they rely on smarter operations.

Instead of solving isolated problems, they optimize the complete service lifecycle.

From receiving a complaint to dispatching technicians, managing spare parts, recording work completed, renewing Annual Maintenance Contracts (AMCs), and analyzing performance, every step is connected.

Let’s examine the strategies that make this possible.

Read More: The Hidden Relationship Between Inventory and Customer Satisfaction

Strategy #1: Eliminate Time Lost in Manual Job Scheduling

Why Scheduling Has Become a Hidden Productivity Killer

Every service request requires decisions:

  • Which technician should be assigned?
  • Who has the necessary skills?
  • Who is closest to the customer?
  • Who has the required certifications?
  • Which technician already has similar jobs nearby?
  • Are spare parts available before dispatch?

When scheduling relies on spreadsheets, WhatsApp messages, phone calls, or whiteboards, valuable time is lost before a technician even begins traveling.

Poor scheduling often results in:

  • Multiple technicians visiting the same area separately
  • Longer travel distances
  • Missed appointments
  • Uneven workload distribution
  • Increased fuel costs
  • Customer delays

Over time, these inefficiencies compound into thousands of lost productive hours.

How Industry Leaders Improve Scheduling

High-performing elevator companies automate scheduling based on operational priorities rather than manual decisions.

Instead of simply assigning the next available technician, they consider:

  • Technician expertise
  • Geographic proximity
  • Job priority
  • Customer SLA commitments
  • Current workload
  • Planned maintenance schedules
  • Emergency service requests

This enables dispatchers to manage larger service volumes while reducing administrative effort.

The result isn’t just faster scheduling—it creates more productive hours for the entire workforce.

Strategy #2: Give Field Technicians Complete Service Visibility

Information Delays Create Service Delays

A technician arriving on-site without the right information creates unnecessary problems.

They may need to:

  • Call the office
  • Request customer history
  • Confirm warranty details
  • Check previous repairs
  • Verify maintenance records
  • Ask whether replacement parts are available

Each interruption increases repair time.

In some cases, technicians must revisit the same site because they lacked the necessary information during the initial visit.

These repeat visits increase costs while frustrating customers.

What Leading Companies Do Instead

Modern elevator service organizations ensure technicians have immediate access to:

  • Complete service history
  • Installation details
  • Previous complaints
  • Maintenance checklists
  • Equipment specifications
  • Warranty information
  • Customer notes
  • Spare part availability
  • Digital service documentation

When technicians arrive prepared, they diagnose issues more quickly and resolve them with greater confidence.

This significantly improves first-time fix rates while reducing administrative back-and-forth.

Strategy #3: Prevent Spare Parts from Becoming Service Bottlenecks

The Hidden Cost of Inventory Uncertainty

Many elevator service delays have little to do with technician skills.

The real issue is missing inventory.

A technician may identify the fault within minutes, only to discover that the required spare part:

  • Isn’t available
  • Is stored at another warehouse
  • Was reserved for another project
  • Hasn’t been ordered yet
  • Has inaccurate stock records

The service visit ends without resolving the issue.

Another visit must be scheduled later.

The customer experiences unnecessary downtime.

The technician’s productivity drops despite performing their job correctly.

How Leading Companies Manage Spare Parts

Successful organizations connect inventory directly with service operations.

Before assigning work, they know:

  • Which spare parts are required
  • Where inventory is located
  • Expected delivery timelines
  • Alternative compatible components
  • Current purchase orders
  • Warehouse availability

Instead of discovering shortages at the customer site, they resolve inventory issues beforehand.

This reduces repeat visits while increasing technician productivity.

More importantly, it improves customer confidence because repairs are completed faster.

Strategy #4: Shift from Reactive Repairs to Preventive Maintenance

Emergency Service Is the Most Expensive Service

Many companies spend most of their resources responding to breakdowns.

Unfortunately, emergency repairs often involve:

  • Higher travel costs
  • Customer dissatisfaction
  • Overtime expenses
  • Technician schedule disruptions
  • SLA penalties
  • Increased operational pressure

The more emergencies occur, the less time technicians have for planned maintenance.

Eventually, preventive maintenance gets delayed, creating even more emergency breakdowns.

It’s a costly cycle.

How Leading Elevator Companies Break the Cycle

Rather than waiting for failures, high-performing companies prioritize preventive maintenance based on:

  • Service intervals
  • Equipment age
  • Usage patterns
  • Maintenance history
  • Inspection findings
  • Compliance schedules

Planned maintenance helps identify worn components before they fail, reducing emergency calls and allowing technicians to work on structured schedules instead of constantly reacting to unexpected issues.

The long-term result is greater equipment reliability, more predictable workloads, and improved customer satisfaction.

Operational Excellence Is Built on Connected Processes

Although these four strategies may seem independent, they are closely connected.

Efficient scheduling depends on technician availability, service history, and customer priorities.

Successful preventive maintenance relies on accurate maintenance records and timely planning.

First-time fixes depend on technicians having the right information and the right spare parts before arriving on-site.

When these processes operate in isolation, productivity suffers. When they work together, the same workforce can accomplish significantly more with less effort.

This is one of the defining characteristics of leading elevator companies: they don’t simply optimize individual tasks—they build connected service operations where information flows seamlessly across departments.

Strategy #5: Standardize Every Service Visit

One of the biggest differences between average-performing elevator companies and industry leaders is consistency.

When service quality depends entirely on individual technician experience, results become unpredictable.

Some technicians follow every inspection step carefully. Others may skip non-critical checks to save time, especially during busy periods. Over time, these inconsistencies can lead to recurring faults, customer complaints, and safety concerns.

Why Standardization Matters

A standardized service process ensures that every technician follows the same best practices regardless of experience.

This includes:

  • Equipment inspection checklists
  • Safety verification procedures
  • Lubrication schedules
  • Component testing
  • Photo documentation
  • Digital customer signatures
  • Compliance records

Instead of relying on memory or handwritten notes, technicians complete structured inspections that become part of the equipment’s service history.

The result is higher service quality, fewer missed inspection points, and improved regulatory compliance.

Strategy #6: Reduce Administrative Work for Technicians

Every minute spent filling out paperwork is a minute not spent servicing elevators.

Many organizations still require technicians to:

  • Complete paper service reports
  • Call the office for updates
  • Submit handwritten timesheets
  • Prepare manual expense reports
  • Record travel details separately
  • Return to the office to submit documents

These administrative tasks consume valuable hours every week.

Digital Field Operations Improve Productivity

Leading elevator companies simplify these processes using mobile technology.

Technicians can:

  • Receive service requests instantly
  • Update job status in real time
  • Capture photographs
  • Record customer approvals digitally
  • Generate service reports on-site
  • Log travel and working hours
  • Update equipment condition
  • Request spare parts immediately

Instead of spending evenings completing paperwork, technicians finish documentation while still at the customer location.

This improves productivity while giving management real-time visibility into ongoing service operations.

Strategy #7: Use Data to Improve Decisions Instead of Guesswork

Many service organizations collect large amounts of data but rarely use it effectively.

Information remains scattered across spreadsheets, accounting software, service applications, and email conversations.

Without meaningful insights, management often relies on assumptions.

Questions such as these become difficult to answer:

  • Which technicians complete the most jobs successfully?
  • Which elevators generate the highest maintenance costs?
  • Which customers require repeated emergency visits?
  • Which spare parts fail most frequently?
  • Which AMCs are least profitable?
  • Where are service delays occurring?

Without accurate reporting, operational improvements become reactive rather than strategic.

High-Performing Companies Measure Everything

Leading organizations continuously monitor key performance indicators (KPIs), including:

Technician Productivity

  • Jobs completed per day
  • Average response time
  • First-time fix rate
  • Travel hours
  • Utilization percentage

Customer Service Metrics

  • Complaint resolution time
  • SLA compliance
  • Customer satisfaction
  • Repeat service requests

Operational Performance

  • Preventive vs. breakdown maintenance ratio
  • Spare parts consumption
  • Inventory turnover
  • Maintenance backlog

These insights help management identify trends before they become costly problems.

Instead of asking, “What went wrong?” they begin asking, “How can we prevent it?”

Strategy #8: Automate Annual Maintenance Contract (AMC) Management

AMCs represent a significant source of recurring revenue for elevator companies.

Yet many businesses still manage renewals manually.

Sales teams rely on spreadsheets to track renewal dates.

Follow-up reminders are missed.

Proposals are delayed.

Customers receive renewal quotations after contracts have already expired.

Every missed renewal represents lost revenue.

How Leading Elevator Companies Protect Recurring Revenue

Rather than depending on manual tracking, successful organizations automate the entire AMC lifecycle.

This includes:

  • Contract reminders
  • Renewal notifications
  • Automated proposal generation
  • Customer communication
  • Service scheduling
  • Billing
  • Contract performance tracking

Automation ensures that no contract is forgotten while allowing service teams to focus on delivering value instead of managing paperwork.

The result is stronger customer retention and more predictable revenue.

Strategy #9: Connect Service with Inventory, Procurement, and Finance

Many elevator companies operate separate systems for:

  • Customer management
  • Service operations
  • Inventory
  • Procurement
  • Accounting
  • Payroll

Each department maintains its own records.

Information must be transferred manually between systems.

This creates delays, duplicate work, and frequent errors.

The Cost of Disconnected Departments

Consider a common service scenario.

A technician identifies a faulty drive unit during maintenance.

The service department raises a request.

The procurement team doesn’t see it immediately.

Inventory records are outdated.

The purchase order is delayed.

Finance hasn’t approved the supplier payment.

The replacement part arrives late.

The customer waits several more days.

Although every department completed its own task, the overall customer experience suffers.

Connected Operations Deliver Faster Service

Leading companies remove these barriers by connecting every department into a single operational workflow.

Instead of isolated systems:

  • Service requests automatically generate spare parts requirements.
  • Inventory updates instantly after material consumption.
  • Procurement receives purchase requirements immediately.
  • Finance tracks costs in real time.
  • Management monitors the complete service lifecycle from one platform.

This eliminates unnecessary communication delays while significantly improving operational efficiency.

Read More: How Much Revenue Are Elevator Companies Losing Due to Poor Scheduling?

The Common Thread Behind High-Performing Elevator Companies

Although the previous strategies cover different areas of the business, they all have one thing in common.

They depend on connected information.

Scheduling becomes smarter when technician availability, customer priority, and service history are visible together.

Inventory planning becomes more accurate when maintenance schedules and spare parts consumption are linked.

Customer service improves when technicians have complete equipment history before arriving on-site.

Finance gains better cost visibility when every service activity automatically updates project and operational expenses.

Without connected data, every department optimizes only its own work.

With connected data, the entire organization works toward the same objective: delivering faster, more reliable service.

Why Spreadsheets and Multiple Software Systems Eventually Limit Growth

Many elevator companies begin with separate tools because they solve immediate problems.

One application manages accounting.

Another handles inventory.

Service requests are tracked in spreadsheets.

Customer communication happens through email and messaging apps.

Initially, this seems manageable.

However, as the customer base grows, these disconnected systems create increasing operational complexity.

Common challenges include:

  • Duplicate data entry
  • Conflicting customer information
  • Delayed reporting
  • Inventory inaccuracies
  • Missed maintenance schedules
  • Manual coordination between departments
  • Limited visibility into business performance

Eventually, growth slows—not because demand decreases, but because internal processes cannot scale efficiently.

The Role of Integrated ERP in Modern Elevator Service Operations

The most successful elevator companies no longer view service management as an isolated function.

Instead, they treat it as part of a connected business ecosystem.

Every service activity influences inventory, procurement, finance, customer relationships, workforce planning, and future maintenance schedules.

Managing these processes through disconnected software makes continuous improvement increasingly difficult.

This is where an industry-focused ERP platform creates measurable value.

Rather than replacing individual processes, it connects them into one unified system where information flows automatically between departments.

For elevator businesses, this means:

  • Service teams work with complete customer and equipment history.
  • Spare parts availability is visible before technicians are dispatched.
  • AMC renewals are tracked automatically.
  • Inventory, procurement, and finance stay synchronized.
  • Managers gain real-time operational dashboards instead of waiting for manual reports.
  • Leadership can make faster decisions based on accurate business data rather than assumptions.

ERPbyNet has been designed specifically with project-based engineering and elevator businesses in mind. Instead of offering generic business software, it connects field service, AMC management, inventory, procurement, finance, projects, and customer operations into a single platform, helping companies improve service delivery without proportionally increasing their workforce.

Better Service Isn’t Just Good for Customers—It’s Good for Business

When elevator companies improve operational efficiency, the benefits extend far beyond faster service calls.

Every improvement made in scheduling, inventory management, preventive maintenance, and workforce productivity contributes directly to the company’s financial performance.

Instead of investing heavily in expanding the workforce, businesses begin generating more value from the resources they already have.

The results become measurable across every department.

Higher Technician Productivity

When technicians spend less time waiting for information, searching for spare parts, or traveling unnecessarily, they can complete more productive work during the same working hours.

This enables businesses to:

  • Complete more service calls per technician
  • Increase preventive maintenance coverage
  • Reduce overtime expenses
  • Improve workforce utilization
  • Handle business growth without immediately hiring additional staff

Improved Customer Satisfaction

Customers rarely judge service providers only by technical expertise.

They value reliability, communication, and speed.

An organized service operation helps businesses deliver:

  • Faster complaint resolution
  • Accurate service scheduling
  • Better communication
  • Higher first-time fix rates
  • Consistent preventive maintenance
  • Reduced equipment downtime

Satisfied customers are also more likely to renew Annual Maintenance Contracts (AMCs), recommend your services, and trust your company with modernization and installation projects.

Better Financial Control

Disconnected operations often make it difficult to understand the actual cost of delivering services.

Without accurate cost visibility, companies struggle to answer important business questions such as:

  • Which maintenance contracts are profitable?
  • Which customers require excessive service visits?
  • Which spare parts generate the highest expenses?
  • Which technicians require additional training?
  • Where is operational waste occurring?

Connected business systems provide management with real-time financial visibility, helping them make informed decisions rather than relying on assumptions.

Stronger Competitive Advantage

Today’s elevator industry is becoming increasingly competitive.

Customers compare vendors based on:

  • Response times
  • Service quality
  • Maintenance reliability
  • Communication
  • Digital documentation
  • Preventive maintenance capabilities
  • Long-term service performance

Companies that operate efficiently are naturally able to provide a better customer experience while maintaining healthy profit margins.

Operational excellence becomes a competitive advantage that is difficult for competitors to replicate.

Why Integrated Operations Matter More Than Individual Software

Many businesses already use software.

The problem isn’t the absence of technology.

The problem is that different departments often use different systems that don’t communicate with each other.

For example:

  • Customer complaints may be managed in one application.
  • Inventory may be tracked somewhere else.
  • Accounting may use separate software.
  • Purchase requests might be handled through spreadsheets.
  • Service reports may still be maintained manually.

Each system performs its own task.

However, the business itself remains disconnected.

This lack of integration creates delays, duplicate work, inconsistent information, and poor decision-making.

Modern elevator companies are moving away from isolated software tools toward connected business platforms where every department works with the same real-time data.

How ERPbyNet Helps Elevator Companies Deliver Better Service

ERPbyNet elevator ERP software infographic showing centralized service management, intelligent AMC management, connected inventory and spare parts management, and real-time business insights for elevator companies.

Improving service quality isn’t about replacing experienced technicians.

It’s about giving them the right information, tools, and processes to perform at their best.

ERPbyNet has been developed specifically for project-based engineering businesses and the elevator industry, bringing together every critical business function into a single integrated platform.

Instead of switching between multiple systems, your teams work from one centralized source of information.

Centralized Service Management

ERPbyNet helps service teams manage the complete service lifecycle, including:

  • Complaint registration
  • Service request allocation
  • Technician scheduling
  • Job tracking
  • Digital service reports
  • Customer communication
  • Service history
  • Equipment records

Every service activity is recorded, tracked, and easily accessible whenever needed.

Intelligent AMC Management

Recurring maintenance contracts are one of the most valuable revenue streams for elevator companies.

ERPbyNet simplifies AMC operations by helping businesses:

  • Track contract validity
  • Schedule preventive maintenance automatically
  • Generate renewal proposals
  • Monitor SLA compliance
  • Record maintenance history
  • Improve customer retention

This reduces administrative effort while ensuring that valuable renewal opportunities are never overlooked.

Connected Inventory and Spare Parts Management

Service efficiency depends heavily on spare parts availability.

ERPbyNet connects inventory directly with field service operations, helping businesses:

  • Monitor stock levels in real time
  • Reserve materials for service jobs
  • Manage warehouse inventory
  • Generate purchase requirements automatically
  • Reduce emergency procurement
  • Improve spare parts planning

Technicians arrive better prepared, increasing first-time fix rates and reducing unnecessary repeat visits.

Better Decision-Making Through Real-Time Insights

Operational improvements become sustainable only when management has complete visibility into business performance.

ERPbyNet provides actionable dashboards and reports that help monitor:

Service Performance

  • Response time
  • Complaint resolution
  • Technician productivity
  • Pending service requests
  • SLA compliance

Inventory Performance

  • Spare parts consumption
  • Stock availability
  • Material movement
  • Procurement status

Business Performance

  • AMC renewals
  • Revenue trends
  • Project profitability
  • Service costs
  • Operational efficiency

These insights help leadership identify improvement opportunities before they become operational challenges.

The Future of Elevator Service Belongs to Connected Businesses

The elevator industry is changing rapidly.

Customer expectations continue to grow.

Competition is becoming stronger.

Equipment is becoming smarter.

Workforces remain difficult to expand.

In this environment, sustainable growth will not come from simply hiring more technicians.

It will come from enabling existing teams to work more efficiently through better processes, connected data, and intelligent business systems.

Leading elevator companies understand this shift.

Instead of asking:

“How can we hire more technicians?”

They ask:

“How can we help our current technicians accomplish more?”

That mindset creates long-term operational excellence.

ERPbyNet
Deliver Better Lift Service Without Expanding Your Workforce
ERPbyNet helps elevator companies optimize technician scheduling, manage service calls, track spare parts, and improve first-time fix rates using one integrated ERP platform.
Elevator ERP • Field Service Management
Increase productivity with smarter service management using ERPbyNet.

Conclusion

Delivering better elevator service with the same workforce isn’t about expecting employees to work harder.

It’s about removing the inefficiencies that prevent them from performing at their full potential.

When scheduling is optimized, spare parts are available, preventive maintenance is planned, service history is accessible, and every department works from connected data, businesses naturally become more productive.

The result is faster response times, improved customer satisfaction, stronger financial performance, and the ability to scale operations without proportionally increasing workforce costs.

For elevator companies looking to modernize operations, improve service efficiency, and build a connected business, ERPbyNet provides an integrated platform designed specifically for the industry’s operational needs.

Rather than managing service, inventory, procurement, finance, projects, and AMC operations through separate systems, ERPbyNet brings everything together—helping businesses transform operational complexity into a competitive advantage.

Ready to Improve Service Without Expanding Your Workforce?

The most successful elevator companies aren’t simply adding more technicians—they’re building smarter operations.

If your business is looking to improve technician productivity, strengthen AMC management, optimize spare parts planning, and gain complete visibility across service, inventory, procurement, projects, and finance, ERPbyNet can help you build a more connected and efficient operation.

Discover how ERPbyNet helps elevator companies deliver exceptional service while maximizing the productivity of every technician.

Frequently Asked Questions

What is the biggest challenge affecting elevator service productivity?

The biggest challenge is often operational inefficiency rather than a shortage of technicians. Poor scheduling, disconnected systems, inventory delays, and manual processes reduce the number of productive service hours available each day.

How can elevator companies improve service without hiring more technicians?

Businesses can increase productivity by optimizing technician scheduling, automating preventive maintenance, improving spare parts availability, reducing paperwork, and connecting service operations with inventory, procurement, finance, and customer management.

Why is preventive maintenance more effective than reactive maintenance?

Preventive maintenance identifies potential issues before they become major failures. This reduces emergency breakdowns, lowers repair costs, improves equipment reliability, and allows technicians to work on planned schedules instead of constantly responding to urgent service requests.

Why is integrated ERP important for elevator service companies?

An integrated ERP system connects every department—including service, inventory, procurement, finance, projects, and customer management—into one platform. This improves collaboration, reduces manual work, provides real-time visibility, and enables faster, more informed decision-making.

How does ERPbyNet help elevator companies improve service efficiency?

ERPbyNet helps elevator businesses streamline complaint management, technician scheduling, AMC management, preventive maintenance, spare parts planning, inventory control, procurement, project management, and financial operations within a single integrated platform. This enables companies to deliver faster, more reliable service while making better use of their existing workforce.

Name
Verified by MonsterInsights